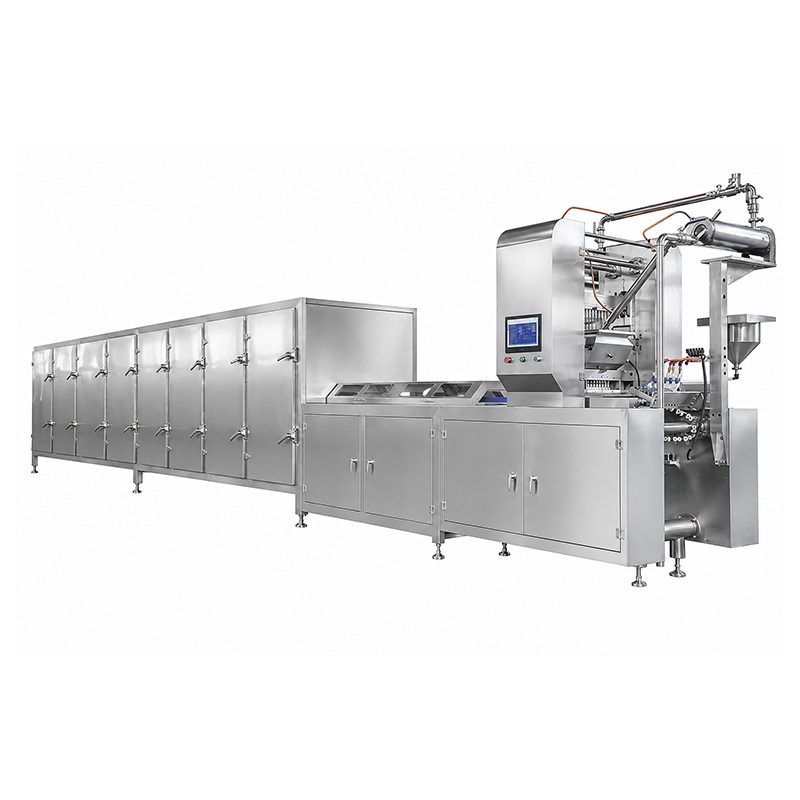
APC-GM300Q Gummy Production Line — 300 kg/h
Multi-shift output with fast recipe and shape changeovers
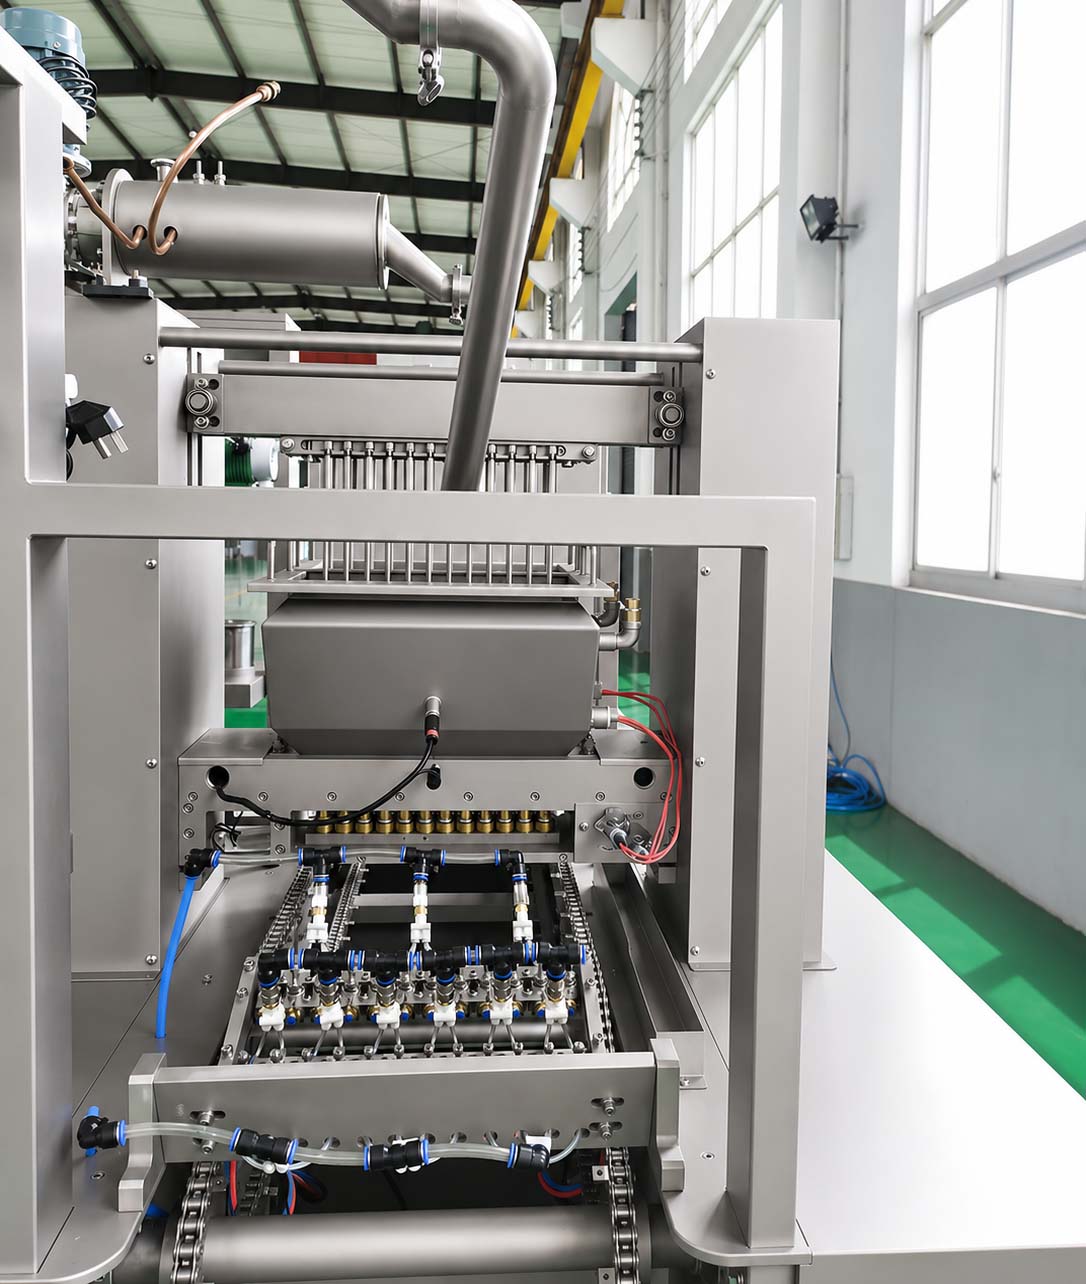
You’re running several recipes for several clients, and the line changes shape more than once a week. The GM300Q runs 300 kilograms an hour with quick-release molds on a guide rail and CIP cleaning built into the frame — so a product change is a wash cycle rather than a teardown.
1.Output — 300 kg/h, 25 to 45 depositing strokes a minute
2.CIP built in — dedicated drain piping in the frame, no teardown between products
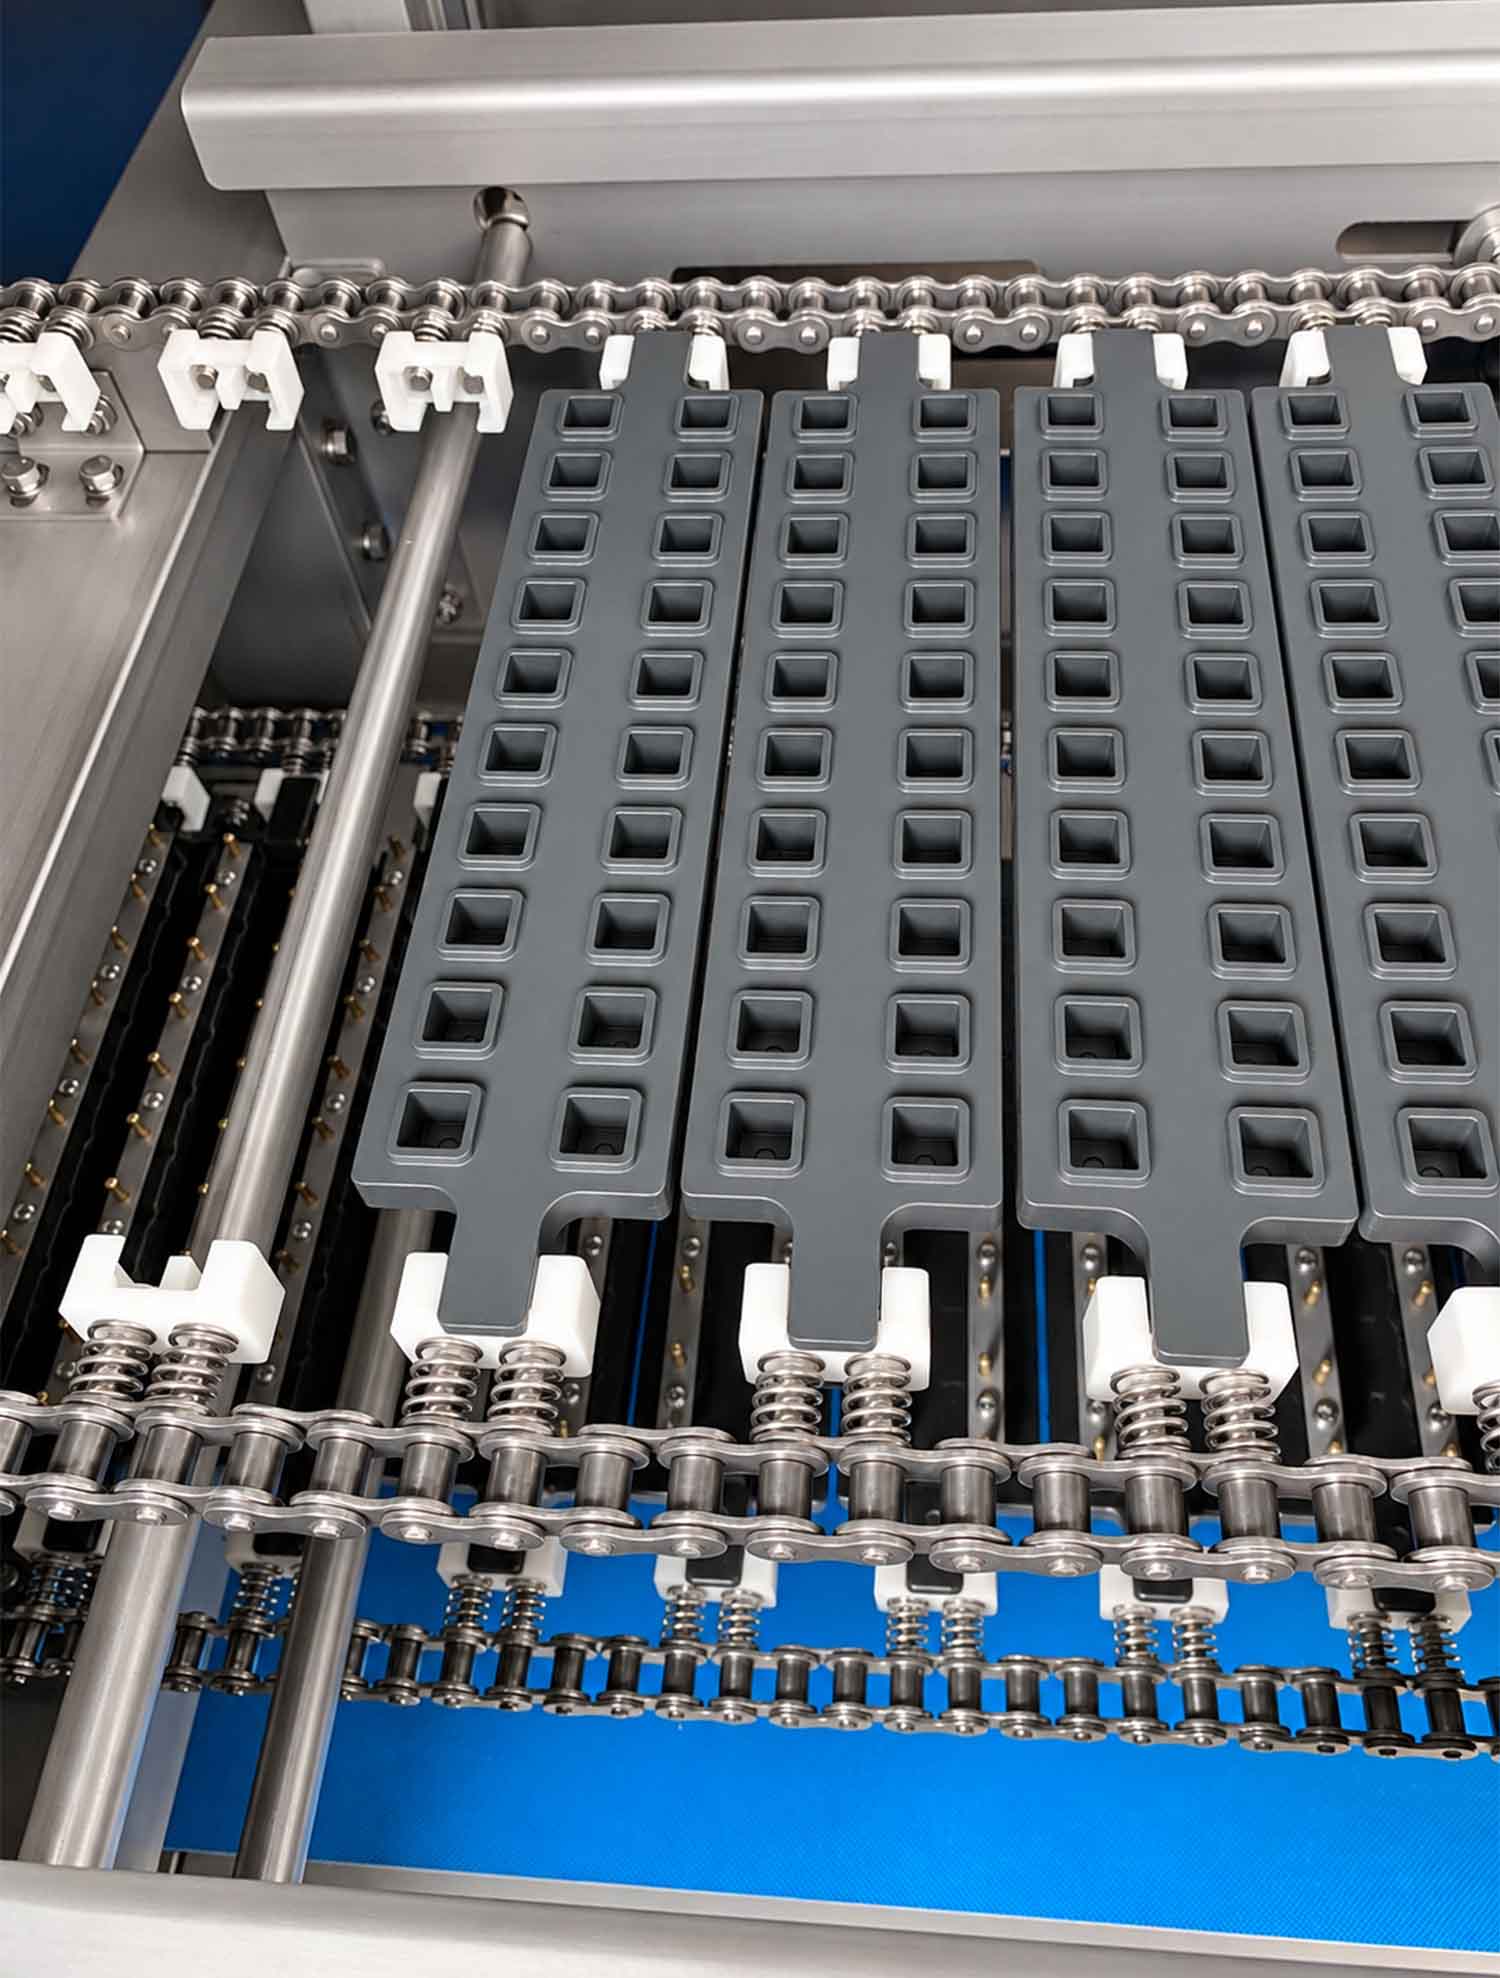
3.Quick-release molds — fast-release buckles on a guide rail, no screws
4.Footprint — 18 m, 75 kW, 300 kg/h steam
Is this the right line for you?
✓ Yes, if…
- You need around 300 kg an hour
- You run multiple recipes or multiple clients
- You change gummy shapes weekly, not yearly
- You have 18 metres, 75 kW and steam at 0.8–1.2 MPa
✕ Buy something else if…
- You run one product continuously → the GM150Q costs less and does the same job at half the output. Changeover speed is what you're paying extra for here
- You need mass-market volumes → see the GM600Q at 600 kg/h
- Your steam pressure is below 0.8 MPa → this line needs more than the smaller ones. Check your boiler before you commit
Quick-Release Molds on a Guide Rail
Molds are fully Teflon-coated and held by fast-release buckles on a guide rail. The alternative is screw-fixed molds with a half coating — an operator, a spanner, and an uncoated area where sticking starts.
CIP Built Into the Frame
Clean-in-place with dedicated drain piping in the machine frame. On a line running several client recipes, a product change is a wash cycle rather than a teardown — which is the difference between changeover being a shift and being an hour.
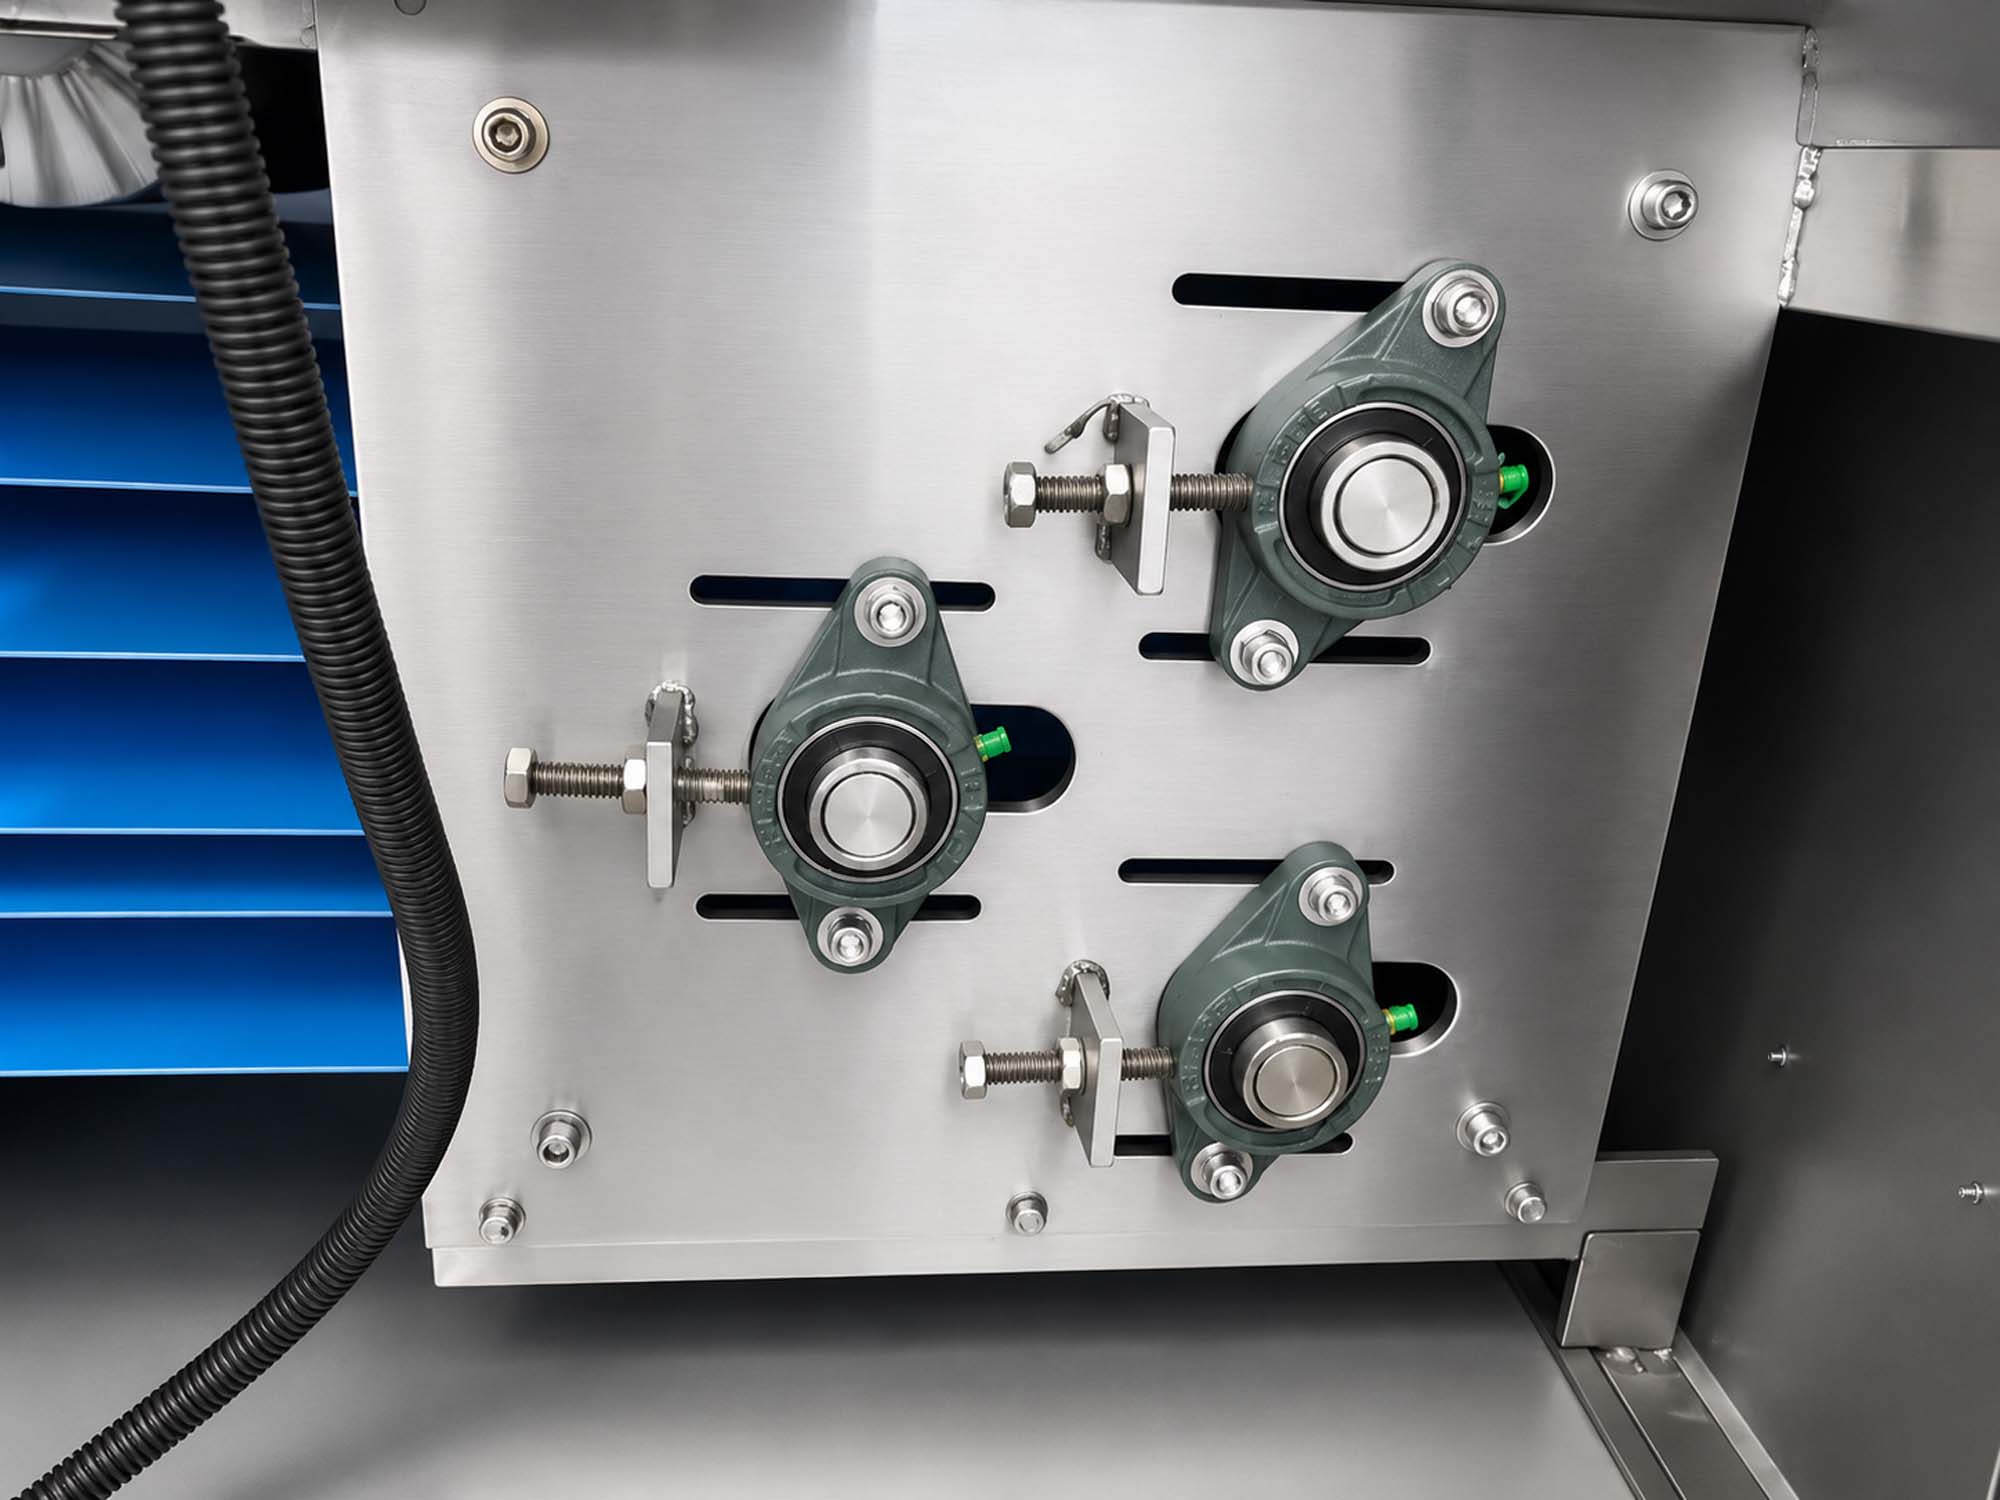
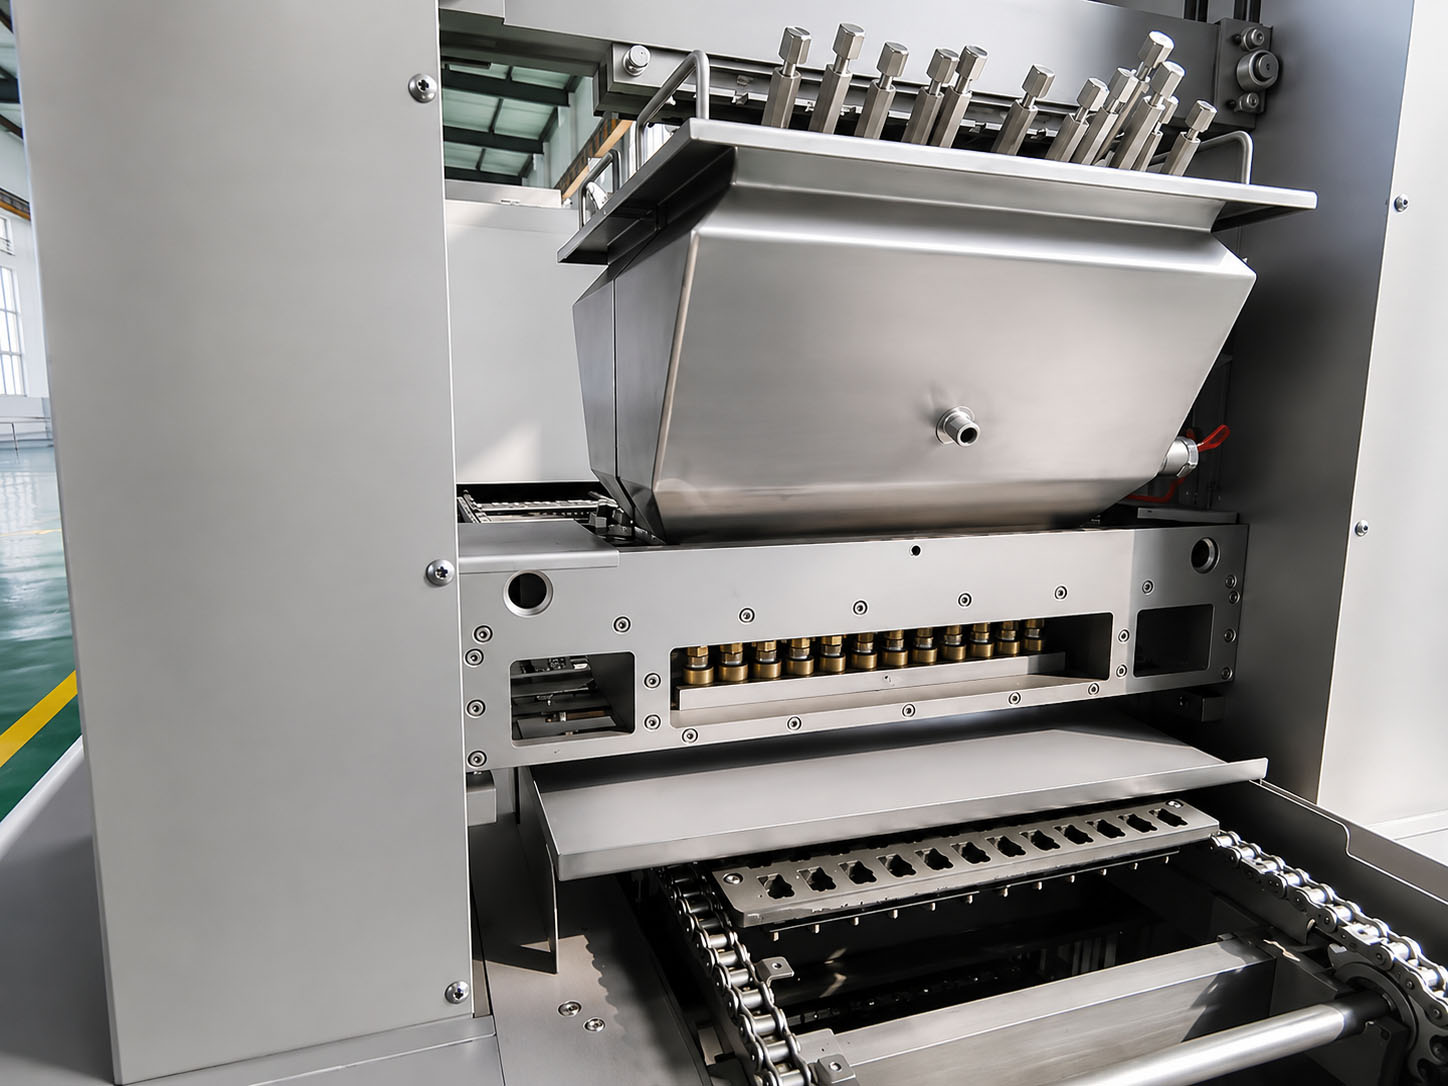
Full-Servo Screw-Driven Depositing
The depositing pistons run on servo motors with solid screw rods and linear guides. Chain-driven depositors are the common alternative — the chain stretches, and fill weight drifts after a few months. That’s a difference you see in your weight checks a year in, not on day one.
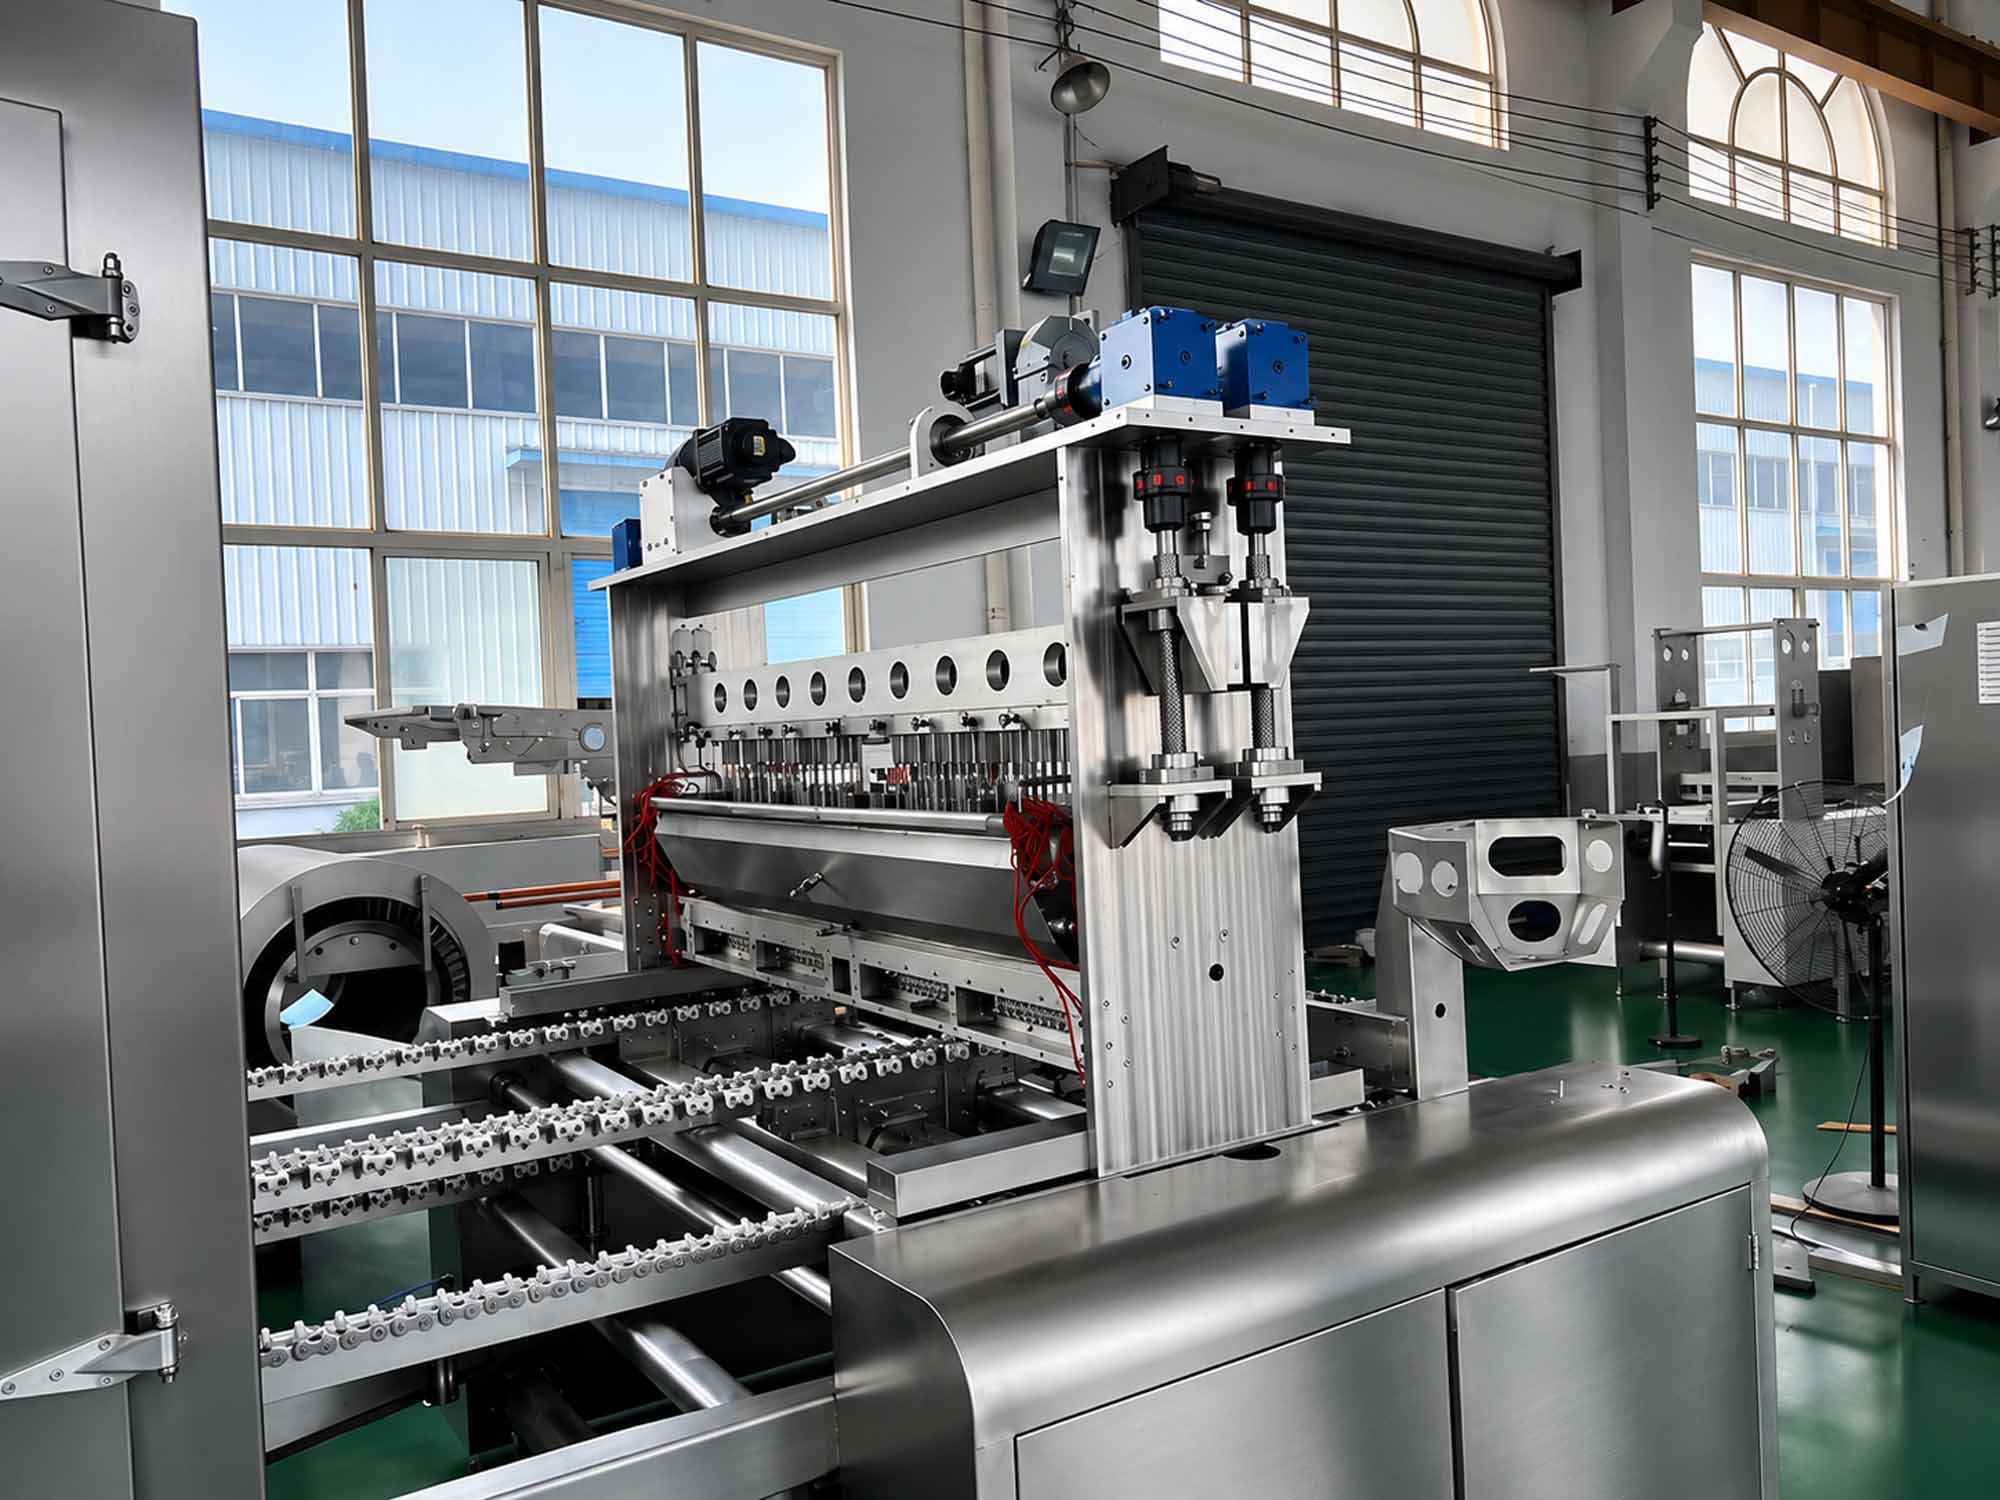
Full-Plate Demolding
Dual pneumatic cylinders drop the whole tray face at once, evenly. The alternative is plate-chain demolding, which grips the frame edges and twists the tray over time — it chips the coating and eventually damages the mold. Two soft rotating brushes finish the release without touching the mold surface.
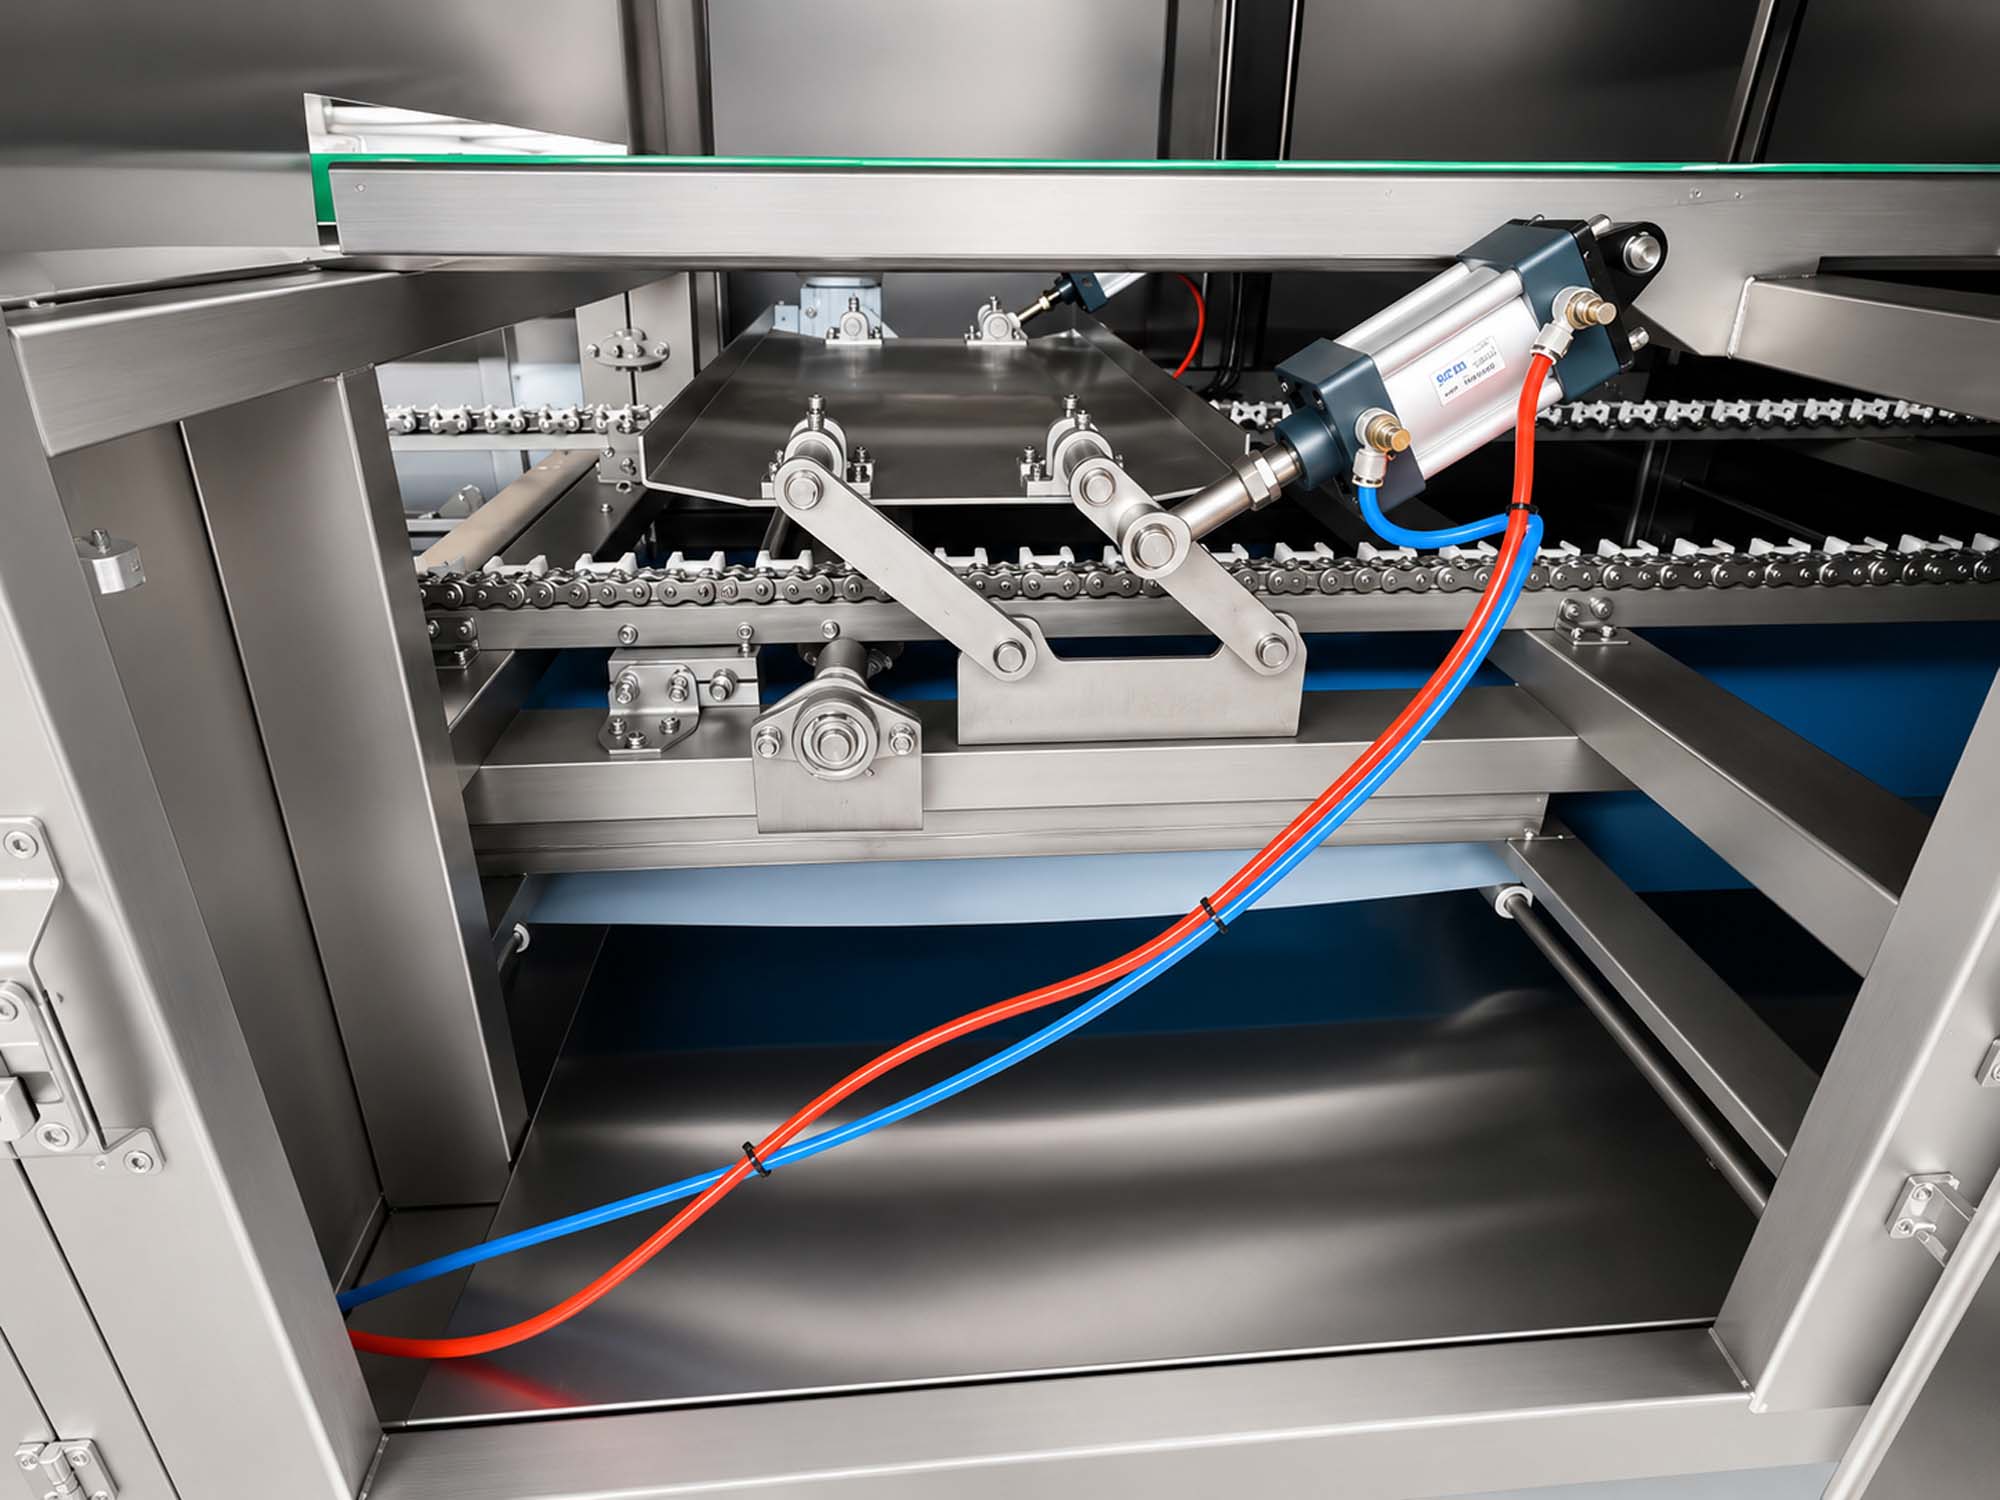
Motor at the Tunnel Exit, Not at the Depositor
The drive motor sits at the cooling tunnel exit and pushes the mold chain rather than pulling it from the front. Front-mounted motors pull the chain unevenly, so over time the chain no longer runs level — and the depositing station loses accuracy because of it.
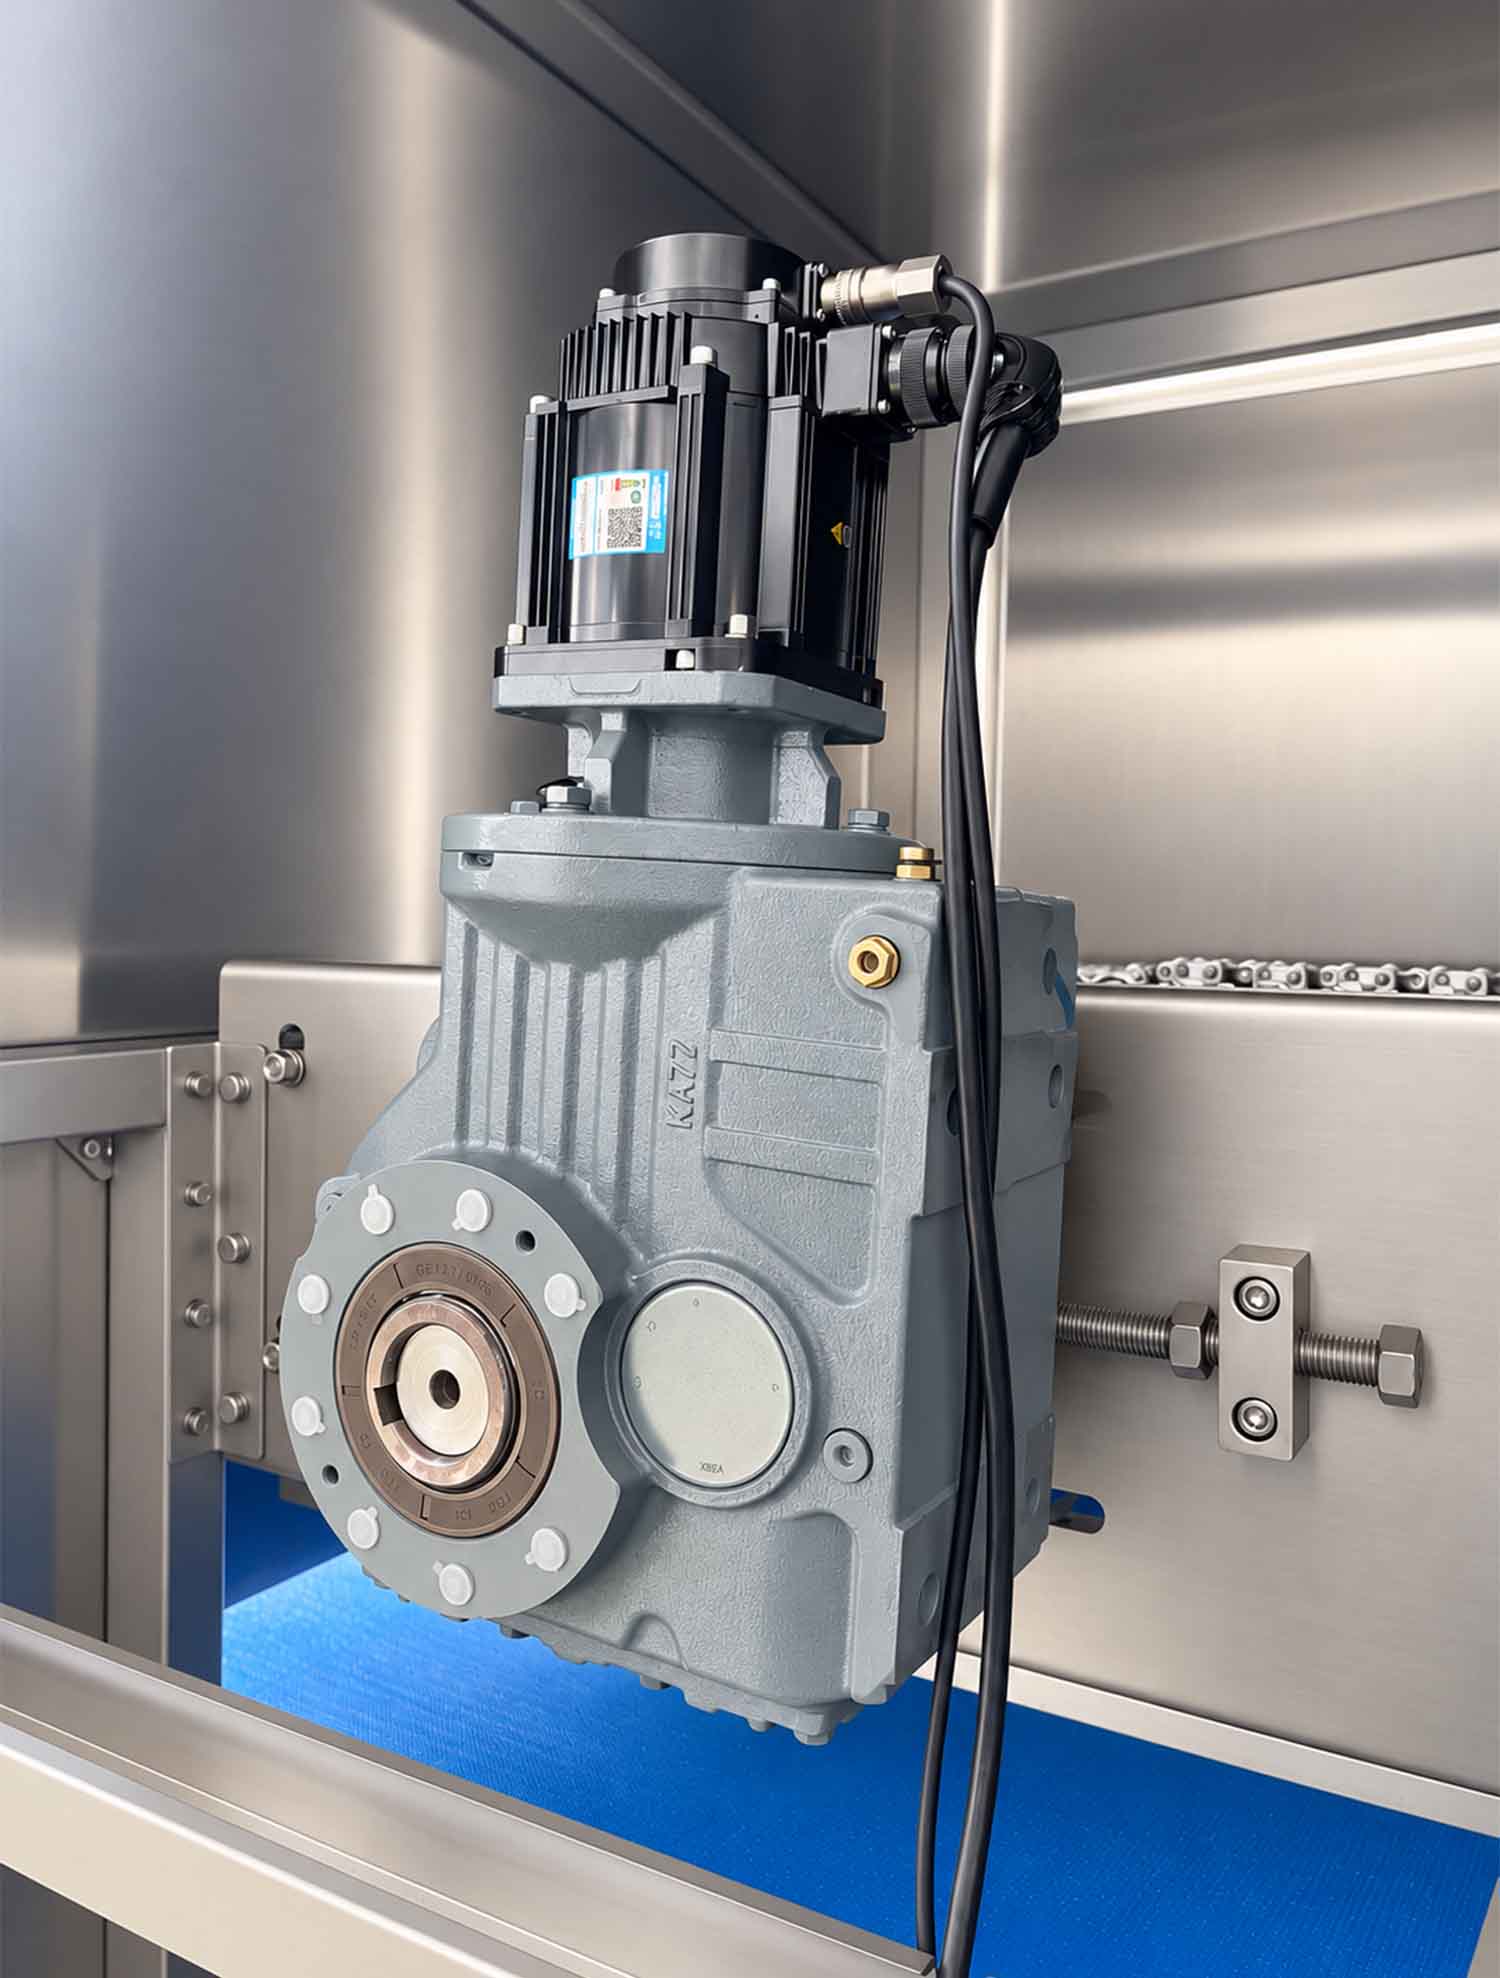
Suspended Belt with Cylinder Tensioning
The blue PU belt runs suspended off the tunnel floor with a pneumatic cylinder holding tension automatically. Belts that sit flush against the tunnel trap spilled syrup underneath — they glue down and they’re hard to clean. Mechanical tensioners wear the belt out faster.
Vertical Dynamic Mixing
Flavour, colour and actives are blended in a vertical mixer rather than a horizontal one. Horizontal mixing lets dense material — mineral powders, botanical extracts, organic acids — settle at the bottom of the pipeline. The vertical design forces the mass upward, and there’s a window so the operator can see it.
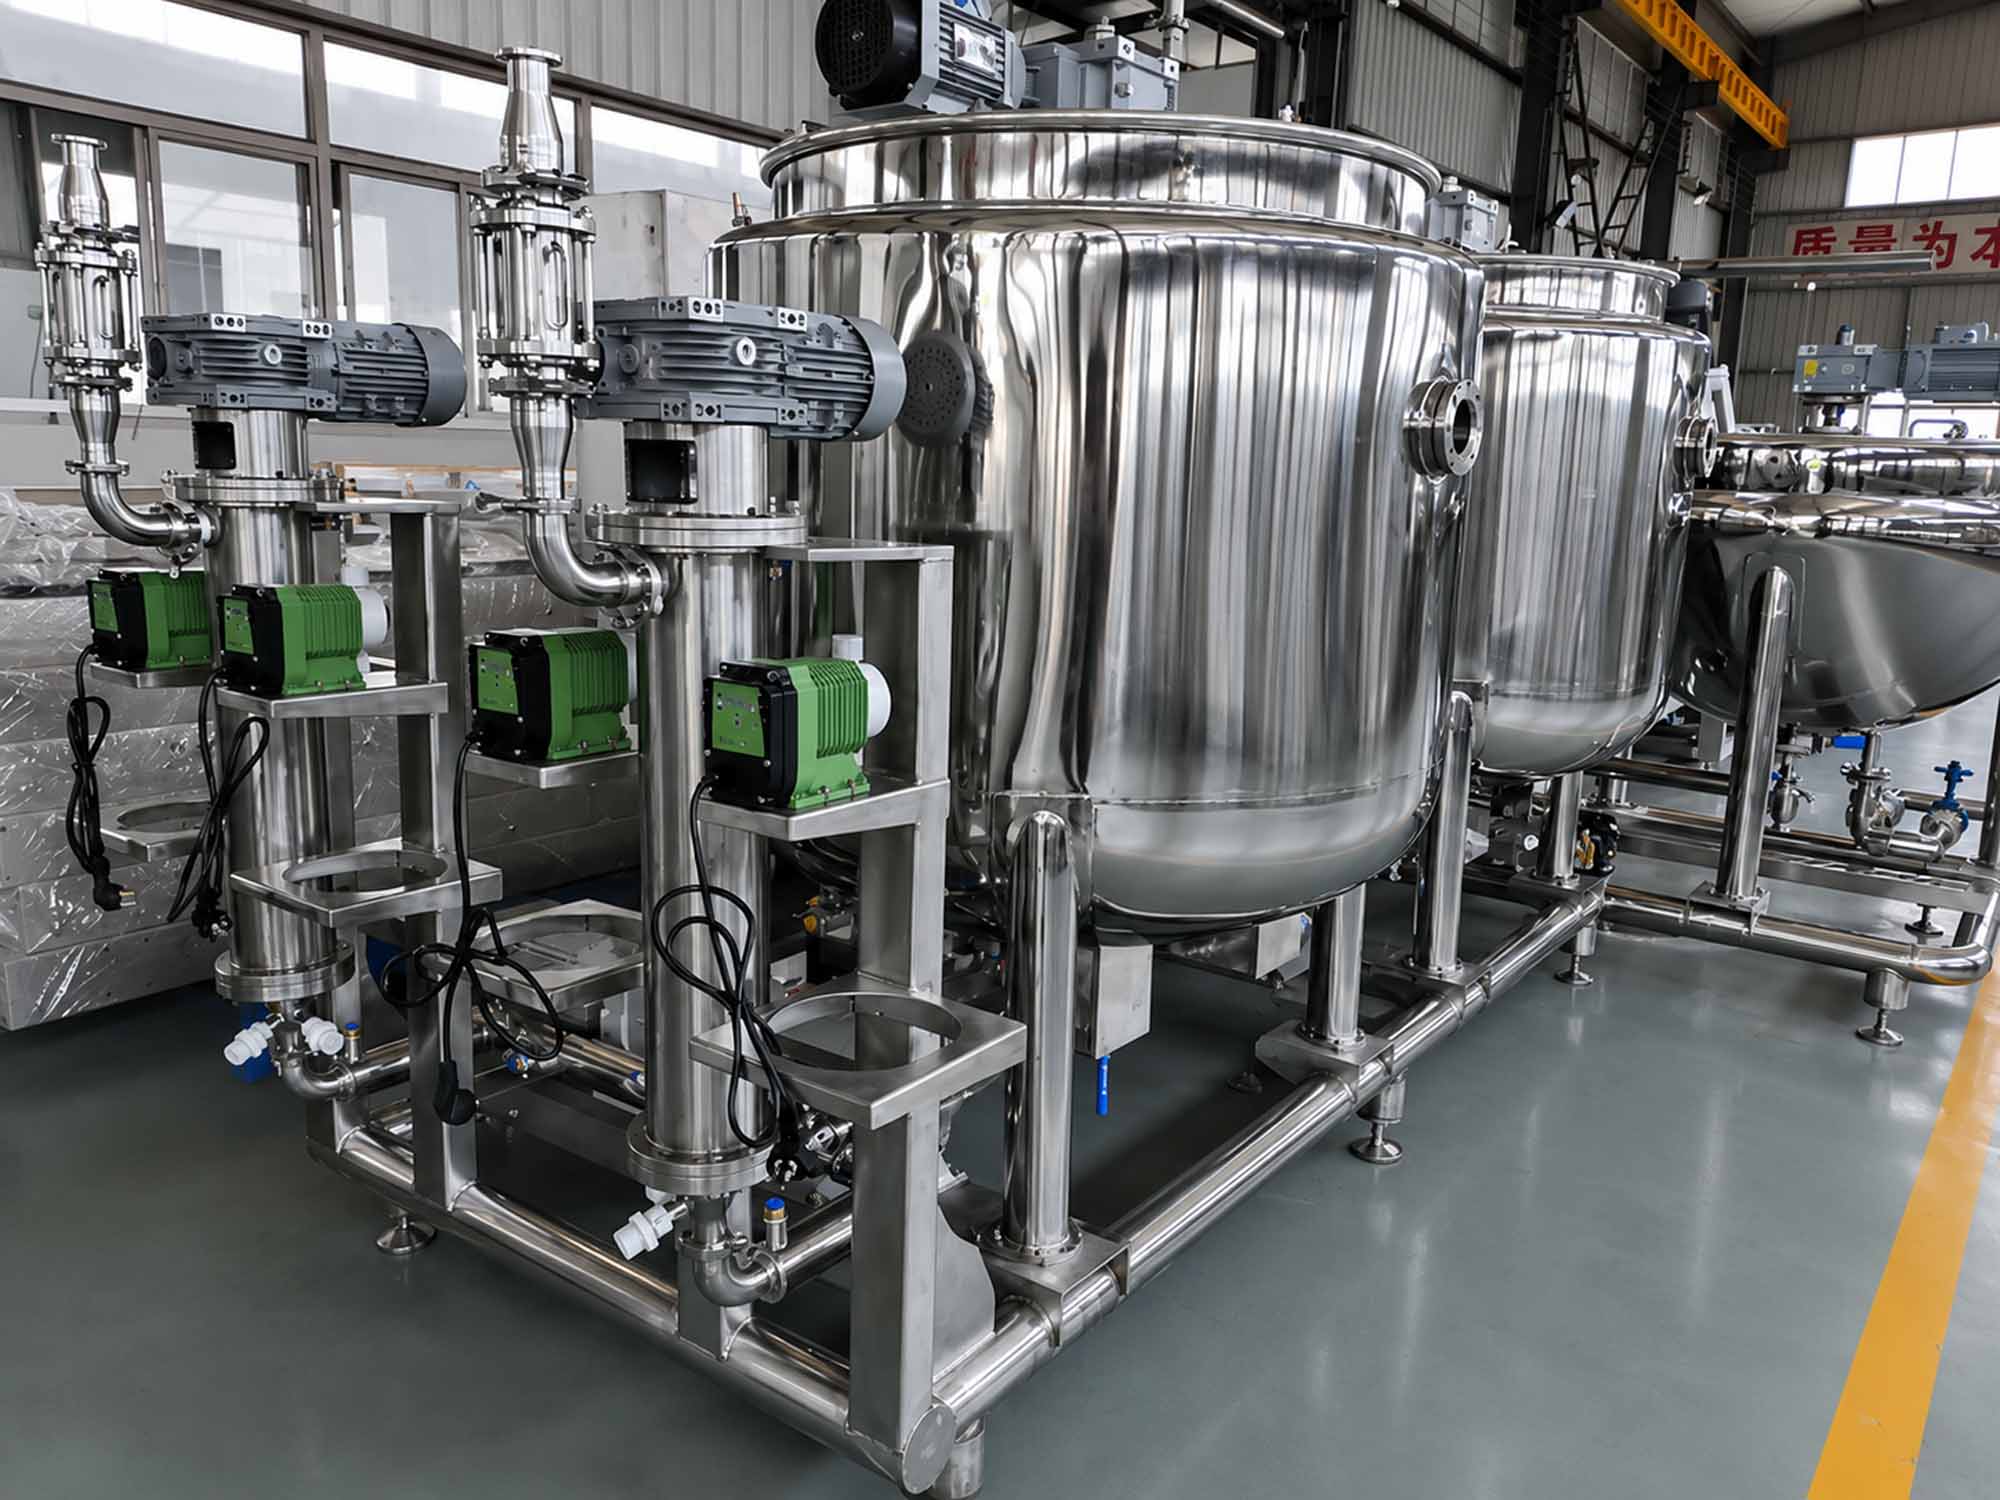
Technical specification
Specification | APC-GM300Q | What it means for you |
Output | 300 kg/h | — |
Depositing speed | 25–45 strokes/min | Slower than the larger lines, which reach 45 |
Dosing accuracy | ≤ ±2% | Same servo depositing as every line we build |
Steam | 300 kg/h at 0.4–0.6 MPa | The lowest steam demand in the range |
Compressed air | 0.2 m³/min at 0.8–1.2 MPa | — |
Installed power | 75 kW, 380 V | Lowest in the range 60 Hz / 480 V |
Room conditions | 25–30 °C, humidity ≤45% | Same at every scale |
Line length | 18 m | Half the GM150Q |
Machine weight | 4,500 kg | — |
Operators | 2–3 | Same as the larger lines — people don’t scale down |
Contact parts | SUS316L | Frame and pipework SUS304 |
Control system | Siemens PLC, UL or CE certified components | — |
Model comparison
Model | Output | Depositing speed | Steam | Power | Line length | Best for |
APC-GM80Q | 80 kg/h | 25–35/min | 80 kg/h, 0.4–0.6 MPa | 55 kW | 8 m | Bringing your first gummy in-house |
APC-GM150Q | 150 kg/h | 25–45/min | 250 kg/h, 0.5–0.8 MPa | 65 kW | 16 m | Growing brands scaling past a co-packer |
APC-GM300Q | 300 kg/h | 25–45/min | 300 kg/h, 0.8–1.2 MPa | 75 kW | 18 m | Multi-shift plants and contract manufacturers |
APC-GM600Q | 600 kg/h | 25–45/min | 500 kg/h, 1.6–1.8 MPa | 85 kW | 20 m | Mass-market confectionery volumes |
Output is in kilograms per hour, not pieces — piece count depends on your gummy weight. Tell us both and we’ll work it back for you.
All four run the same servo depositing, the same full-plate demolding and the same mold system. What changes is throughput, and what that costs you in steam, power and floor.
Industry Applications
Vitamin and mineral gummies
Pectin and vegan formulations
Functional and botanical gummies
Ashwagandha, elderberry, apple cider vinegar. Dense botanical extracts settle in horizontal mixing lines — that’s what the vertical mixer exists for.
CBD and THC gummies
Dose uniformity is the whole product in this category. The vertical mixer is what keeps a dense active from pooling in the pipeline.
What changing over involves
Changing shape is a mold swap. Changing base is a different conversation.
What changed | What you adjust | Roughly |
Same shape, new flavour or colour | Recipe on the screen, flush the mixer | 30-60mins |
Different gummy shape | Swap the mold trays — quick-release buckles on a guide rail, no screws | 30-60mins |
Gelatin → pectin | Cooling tunnel settings and your drying room. Pectin cures 20–24 hours against 8–12 for gelatin | Not a changeover — a process change |
Different piece weight | Depositing stroke on the servo, and possibly the manifold | 30-60mins |
Molds are fully Teflon-coated and held on a guide rail with fast-release buckles. The common alternative is screw-fixed molds with a half coating — those take an operator and a spanner, and the uncoated area is where sticking starts.
On this line, changeover is what you’re buying. CIP is built into the frame with dedicated drain piping, so a product change is a wash cycle rather than a teardown.
What your plant needs to supply
Utilities
Steam — the volume and pressure depend on the line size, listed in the specification table on each model page. Compressed air. Electricity, water inlet and drainage.
Air handling
Two dehumidifiers — one for the cooling area, one for the packing room. Two air conditioners, same two rooms.
Room conditions
Forming area: 25–30 °C, humidity 45% or below. Cooling tunnel: 5–10 °C. Drying room for pectin: 25–30 °C, humidity 25–45%.
What we supply
The line, the layout drawing, installation, operator training — and the formula if you don't have one.
Two things worth raising early. Steam is the one most buyers overlook — if you don’t have a boiler, tell us and we’ll quote the electric heating option instead. And no machine fixes a room that swings: if you can’t hold the forming conditions yet, say so before you order, not at commissioning.
What to check before you buy
Weight consistency, checked over time
A servo depositor and a chain-driven one both hit spec on day one. Ask any supplier what their fill weight looks like after six months of running, and how they verify it at the factory acceptance test. That's the number that decides your giveaway.
The manual
A clear English manual gets your operator running in a week instead of a month. Ask to see a sample page before you order.
Installation and training
Installed, commissioned, and your people taught to run the line. Ask what's included and what costs extra — the answer varies more between suppliers than the machine price does.
Why Choose AIPAK?
We build it — Our own plant in Wuhan. Not a trading company, and not a rebadged line. Custom mold shapes, nozzle counts and layout changes go through the engineers who make the machine.
Formulas included — Gelatin and pectin production formulas with ingredient ratios and process steps. Free, and yours whether you buy from us or not.
Installation and training — We install it, commission it, and teach your operators.
Lead time — 1-3months. Confirmed in writing with your order.
APK-GM300Q Automatic Gummy Making Machine Comprehensive PDP FAQ
Traditional mixing augers rely on horizontal flow patterns, which naturally allow heavily dense medicinal extracts, active botanicals, and citric acids to settle at the base of the pipeline, creating massive dosage variation across a batch. The APK-GM300Q features a Vertical Dynamic Flavor and Colors Mixer that forces the liquid mass into an upward vortex blend. This active mixing pattern keeps dense actives in suspension through the run, zero-settling concentration uniformity, and operators can monitor fluid consistency in real time through the built-in visible window.
Flexible plastic tube designs are highly prone to kinking, blistering, or micro-fracturing when subjected to constant cleanroom expansion cycles and washdown chemistry. To establish permanent technical stability, the APK-GM300Q loop is fabricated exclusively from rigid stainless steel pipelines. This structural setup delivers non-degrading water flow efficiency, prevents pressure-drop leakage, and withstands intense pharmaceutical-grade cleanroom spray-downs.
Plate chain demolding applies localized pinching forces to the outer frame edges, which twists the mold plate over time, chips the non-stick coating line, and ruins tool OEE. AIPAK’s Full-Plate Mechanical Demolding technology employs dual pneumatic cylinders that push the entire tray surface evenly according to fixed alignment parameters. Working alongside dual rotating soft brushes, it achieves complete candy release while keeping the mold plates safe from structural stress.
Product changeovers for multi-ingredient functional gummies require deep cleanroom washdowns. The APK-GM300Q features an IP65-rated electrical standard and uses water-resistant aviation quick-charge plugs for all critical sensor and heating links. Cleaning crews can safely spray down the frame, the inside of the cooling tunnel, and the hopper assemblies with washing water without risking electrical damage or Siemens PLC faults.
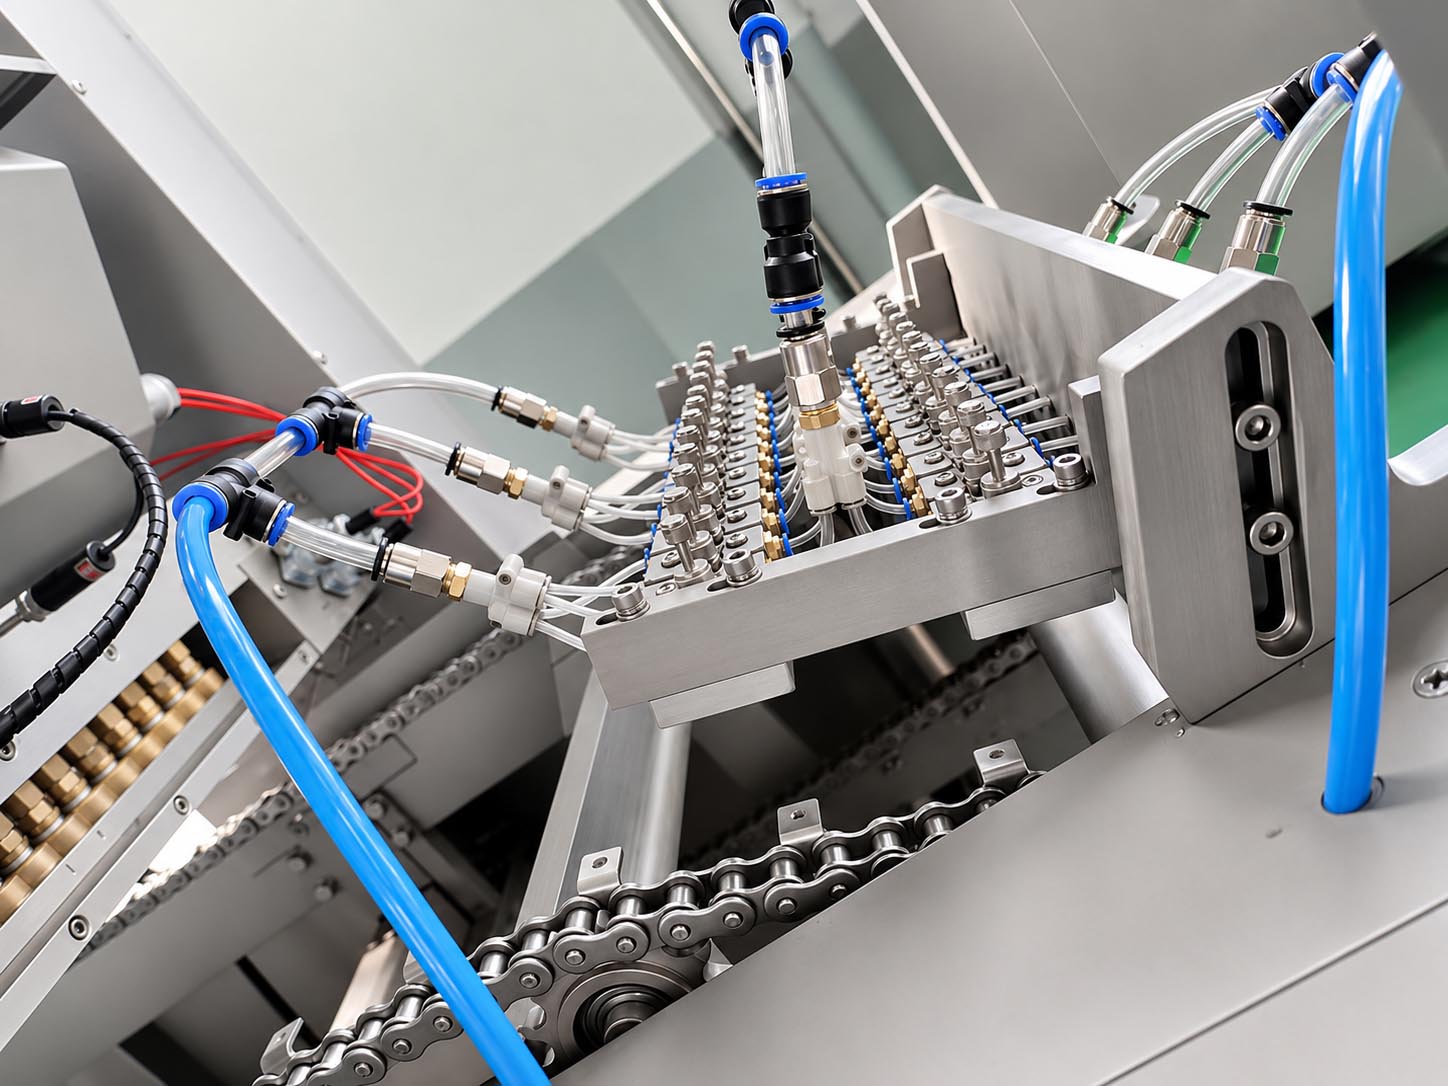
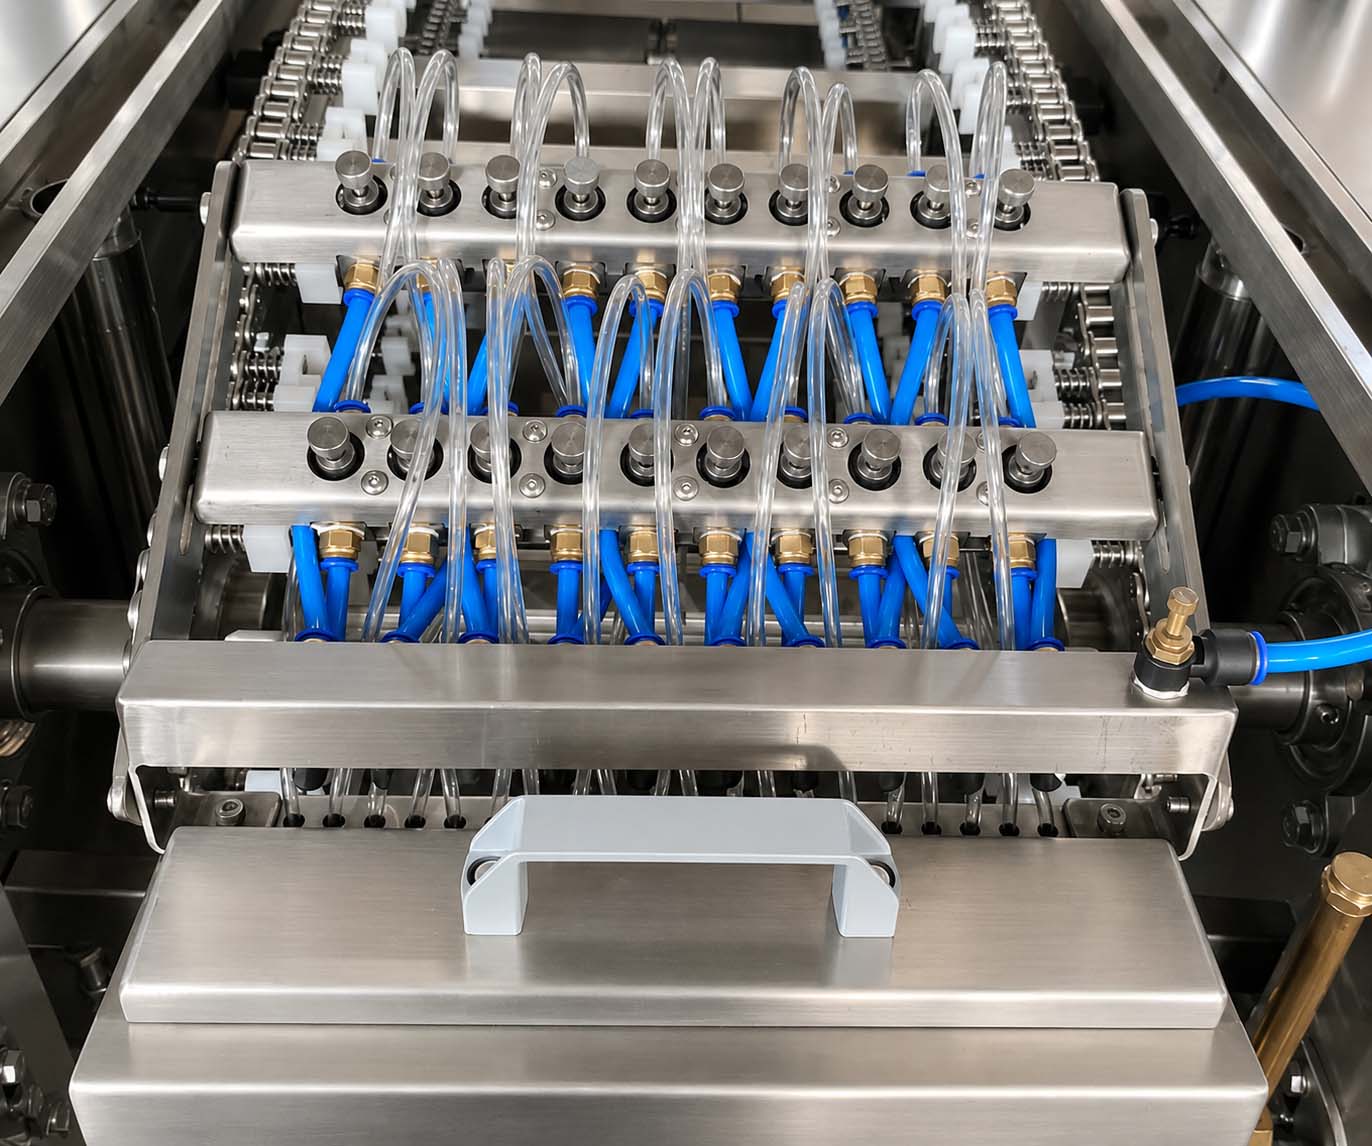
Standard open-valve spray bars lack regulatory pressure controls, forcing operators to constantly adjust the valves manually because of pressure shifts, and often leading to severe oil leaks if the line is forgotten after the shift. Our advanced self-priming oil sprayer uses a solenoid-controlled quantitative nozzle grid. Once set via the micrometer screw adjuster, the atomized volume remains locked and uniform during the entire work cycle, saving release oil while keeping the molds perfectly lubricated.
Yes, free. We’ll send you production formulas for both gelatin and pectin, with ingredient ratios and the process steps. You don’t have to buy from us to have them.
Forming at 25–30 °C with humidity 45% or below. Cooling tunnel at 5–10 °C. For pectin, a drying room at 25–30 °C and 25–45% humidity for 20 to 24 hours. Gelatin cures faster, 8 to 12 hours. If you can’t hold these yet, tell us early — it changes what we’d recommend.
The cooker can be built with electric heating instead. Tell us at enquiry rather than after the quote — it changes the build and the price, and it’s much easier to specify than to retrofit.
Customers Also Interested In...
Expand your oral solid dosage (OSD), nutraceutical, or gummy manufacturing facility by integrating your primary production lines with AIPAK’s industry-proven pharmaceutical process and packaging machinery:
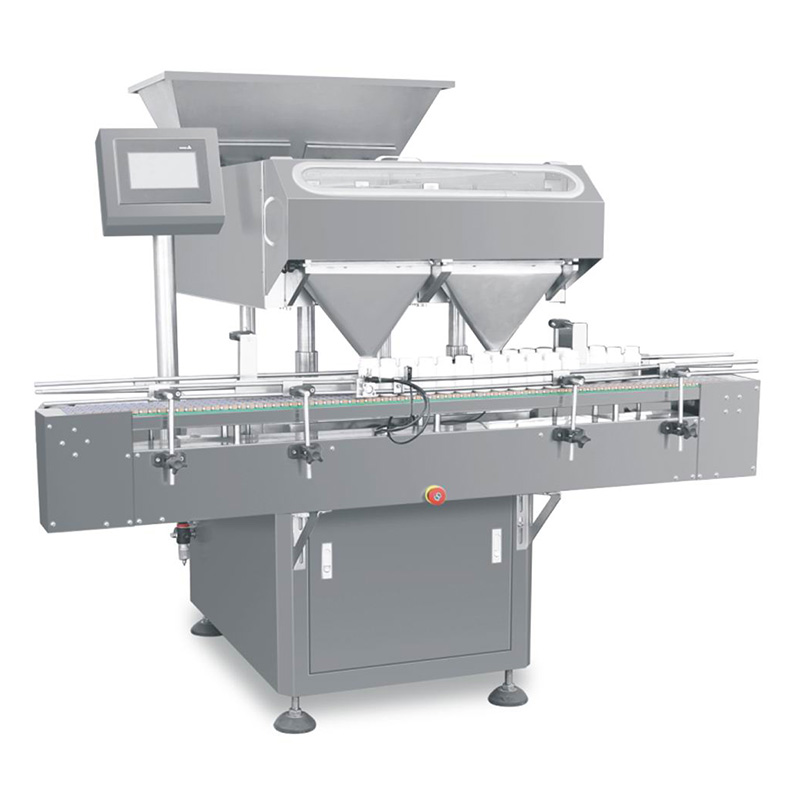
Electronic Gummy Counting Machine
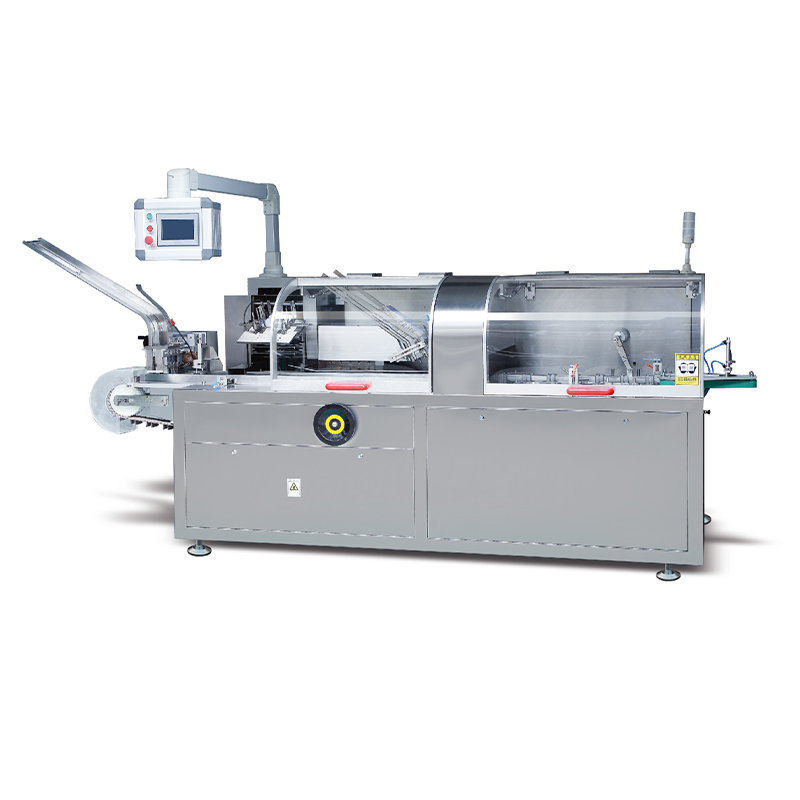
Cartoning Machine
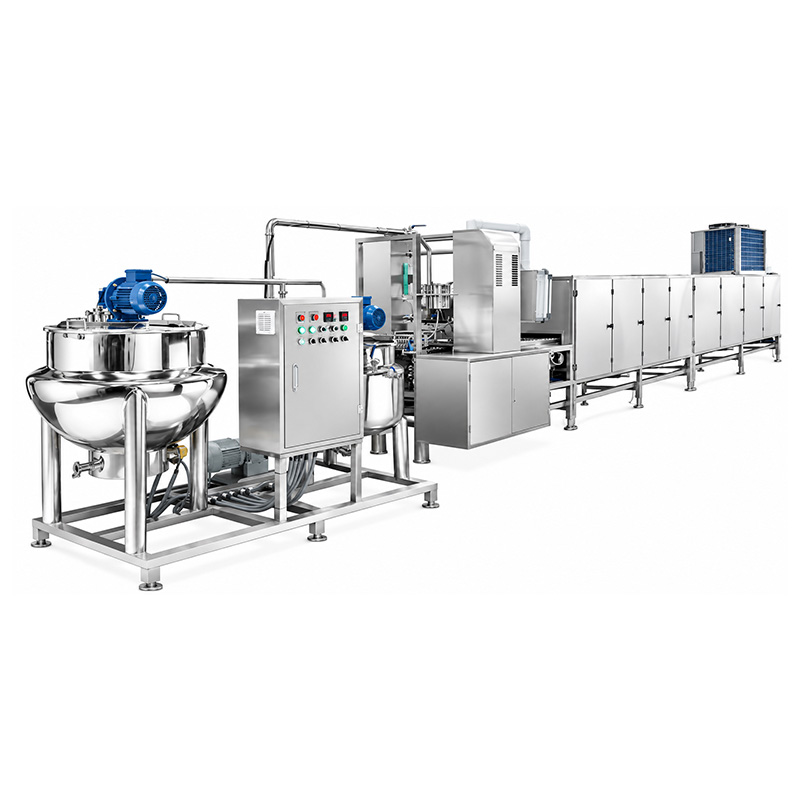
Gummy Line
Not sure which line size?
Tell us your target output in kg per hour and your piece weight. We'll tell you which one, and why.
Send us your formula — or ask us for one
If you have a formula we'll tell you what the line needs to run it. If you don't, we'll send you ours. Free, either way.
Send your floor dimensions
Length, width, height, and where the doors and columns are. We'll draw your line against your actual room.
Reply within one business day. Formulas sent free, whether you buy or not.