Gummy Manufacturing Line
From sugar dissolving to the sealed case — cooking, depositing, cooling, demolding, drying and packing. Tell us your formula base, your piece weight and your daily target, and we’ll tell you which of the four line sizes actually delivers it.
80/150/300/600 kg/h
Depositing output at 2.5–3g per piece
Gelatin/Pectin/Sugar-free
Every rate on this page is depositing output at 2.5–3 g per piece.
Change the piece weight and the number changes. Send us yours and we’ll calculate the real figure, not the brochure figure.
U.S. line: +1 (213) 526-8644 — calls and WhatsApp, Live 8:00–11:00 AM ET, Monday to Friday. Our engineers, not a distributor.
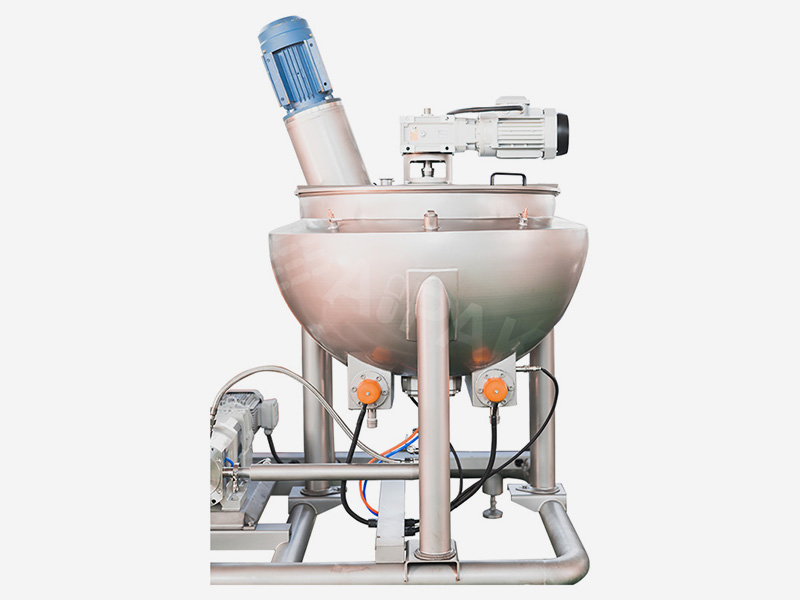
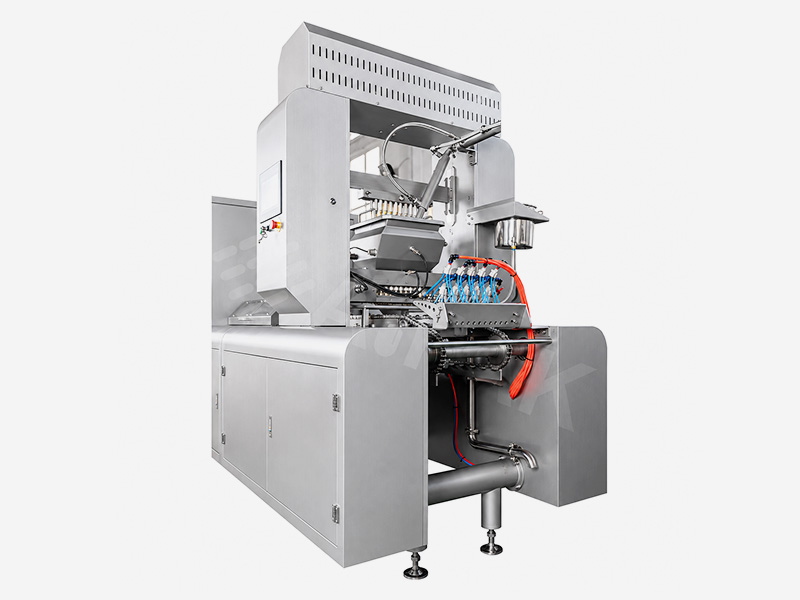
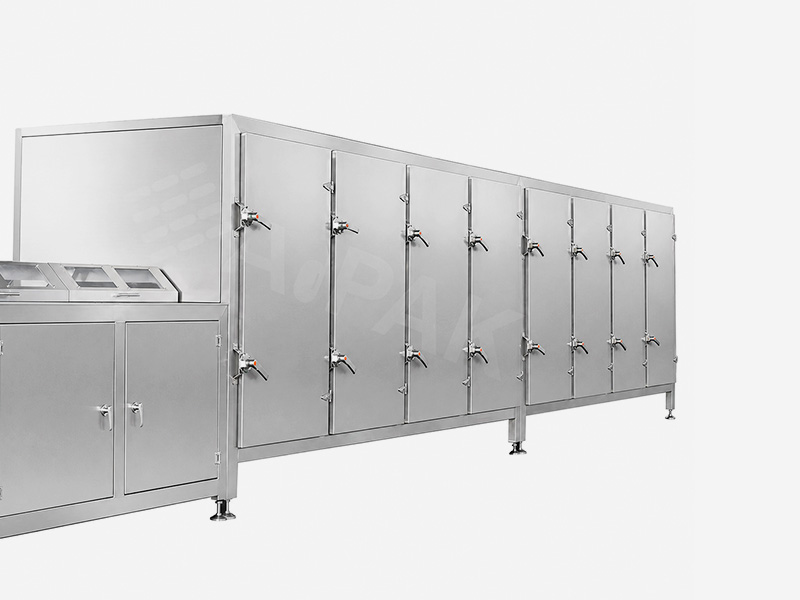
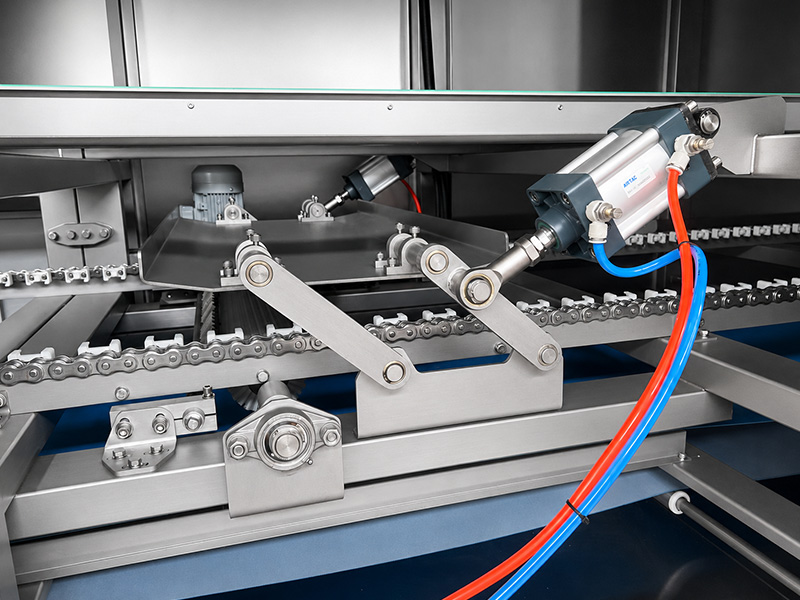
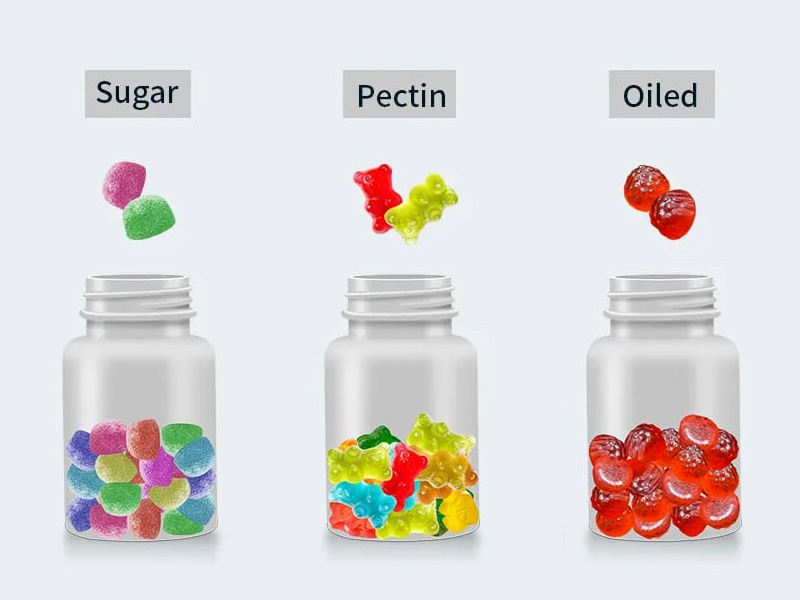
Five stages. We build all of them except the room your gummies dry in
Most gummy quotes cover the first three stages. The two that decide whether you ship on time are the last two.
Sugar, gelatin or pectin dissolving. Screw elevators, dissolving cookers under weighing control, insulated storage tanks, lobe pumps and jacketed transfer lines.
Servo screw depositing, insulated hoppers, mold oiling, quick-release molds, and a cooling tunnel with its own air handling unit.
Full-plate demolding rather than plate-chain, spiral brushes for second release, non-stick PU belt.
We supply the trolleys and the trays. The room itself is yours to build — we tell you exactly what it has to be.
Counted into bottles, or multihead-weighed into pouches. Tray loading and case packing at the end of it.
If a supplier quotes you stages one to three and calls it a line, ask what happens to the product for the 8 hours after it leaves the tunnel.
Four line sizes. Two things decide which one you need
The depositor and the cooling tunnel. Everything else on the line follows from those two.
| Line | Depositing heads | Cooling tunnel | Rated output at 2.5–3 g | Who buys it |
|---|---|---|---|---|
| 80 | 20 | 4 m | 80 kg/h | A first automatic line |
| 150 | 20 | 8 m | 150 kg/h | Where most buyers start |
| 300 | 40 | [8 m] | 300 kg/h | Best output per dollar in the range |
| 600 | 80 | [8 m x2] | 600 kg/h | High volume, or several clients on one line |
Both machines deposit through the same 20 heads. The 150 has an eight-metre cooling tunnel; the 80 has four. The tunnel decides how many mold plates can be cooling at once, and that decides how fast the belt can run without cutting the cooling short. Twice the tunnel, twice the plates per hour, twice the output — from an identical depositor.
So when you put two quotes side by side, don’t compare depositors. Compare tunnels.
It’s what the line makes at 2.5–3 g per piece. Depositing strokes don’t change with piece weight, so a 1.5 g gummy doesn’t come out at half the rate — it comes out lower than that, and it’s harder to hold weight accuracy at the same time. Tell us your piece weight before you compare anything.
The 300 is the one we quote most and the best output per dollar in the range. We’re telling you that even though the 600 is the bigger order. If your volume is genuinely there, take the 600 — but don’t take it to feel safe.
Gelatin, pectin, sugar-free — and what goes in besides the base.
The base sets the process window. What's dosed into it sets the label.
Wide process window, depositing temperature 65°C – 80°C. The forgiving option, and still the majority of what runs in the U.S.
Narrow process window and a distinctly higher depositing temperature 90°C – 105°C. Sensitive to pH and to when the acid goes in. Cooker pairing, temperature control and drying targets are all set up differently from gelatin.
Same process, different inputs — the sugar and glucose syrup are replaced. Yes, applies to all four line sizes.
If you’re running pectin, the question to ask every supplier — including us — is how the temperature is held across the whole depositing circuit, not just in the hopper.
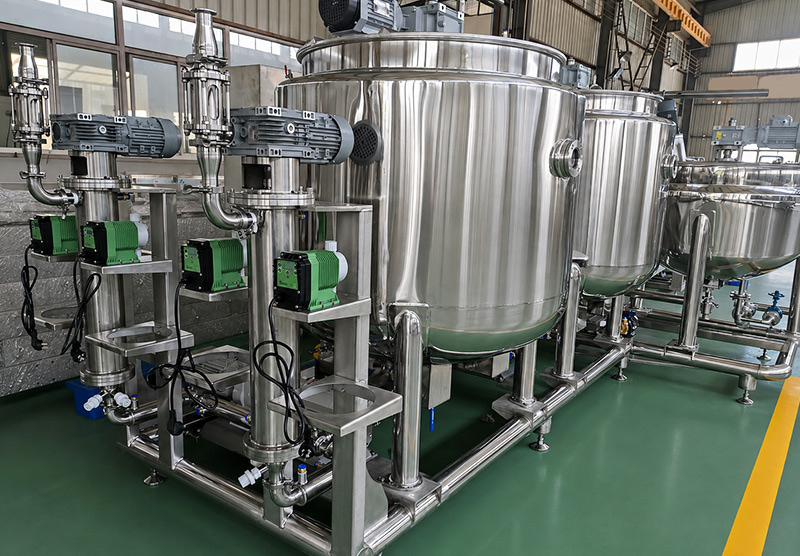
They go in last, in small quantities, at temperature — and they’re what the label is actually about. Our CFA system doses colour, flavour and active ingredients under weighing control, automatically or manually depending on how you want to run the line.
Gelatin and pectin need different cooker pairings, different temperature control and different drying targets, and we can support you on the formula side through recipe adaptation and production scale-up. What we’re accountable for is narrower and more useful: that the same formula gives you the same result on Tuesday that it gave you on Monday.
Your depositor is not your bottleneck. Drying is
Depositing is an hourly rate. Drying is a floor area — and it's the one that caps what you actually ship.
That’s a controlled-environment room, and it belongs to your contractor. Saying so now is cheaper for both of us than finding out on a call.
What we give you instead: the floor area it needs, the temperature and humidity targets for your formula base, and how many trolleys this line will fill.
Most gummy quotes stop at the first line of that calculation. A quote with a kg/h figure and no trolley count is not a line quote.
You're not running one formula. You're running your clients'.
If you're a contract manufacturer, changeover isn't an occasional event — it's most of your week. Here's what changes, and what it costs you in time.
Quick-release molds on a polymer guide rail with fast-release buckles, fully Teflon-coated. Changeover takes less than 30 minutes. Standard feature across all line capacities.
Cookers and tanks carry CIP spray balls and high-shear emulsification. Fully automated CIP hot water washdown cycle in 45–60 mins to eliminate allergen cross-contamination.
Two insulated hoppers, so the same line runs single colour, two-tone or centre-filled without re-plumbing between clients.
Cavities per mold 60–120 cavities · price per set $3,000 – $8,000 · lead time 2–3 weeks.
Decide your shapes early. Mold lead time is the item that most often holds up a line that has otherwise already arrived.
Two numbers hold the label. We control both.
Deposit weight variation is not a cost problem — it's a label claim problem. For a contract manufacturer it's worse than that: the number that fails is printed on someone else's bottle, and it's your name in their supplier file.
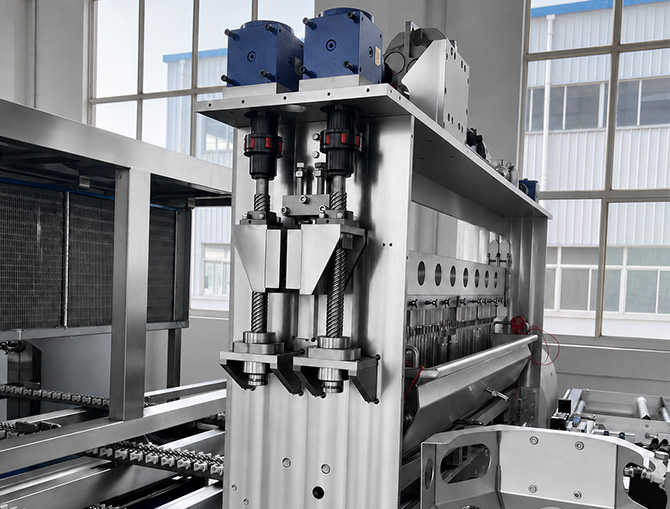
Servo screw depositing under PLC control, with every head depositing the same amount on the same stroke. Accuracy ± 1% based on a standard 3g–5g gummy weight. A chain-driven depositor loses filling precision as the chain wears; ours is servo-driven for exactly that reason.
The CFA system doses colour, flavour and actives under weighing control. That’s where the label claim actually lives — deposit weight only matters because the active rides on it.
Two ways your gummies leave the line.
Gummies are sticky, irregular and rarely uniform, so how you meter them into the pack matters more than it does for tablets. There are two routes, and the one you pick changes the whole back end of the line.
A counting machine meters pieces into each bottle, so the count on the label is the count in the bottle.
Retail supplement packs are sold by count. Weighing gets you close; counting gets you the number that’s printed on the label.
Closures, child-resistant caps, cotton insertion, induction sealing and labelling are covered on the bottling line page rather than repeated here.
We use multihead weighers rather than linear weighers for gummies. Because their combinatorial logic and dimpled contact surfaces prevent the bridging and sticking that typically stall vibratory linear scales.
A rotary premade-pouch machine, or a horizontal form-fill-seal machine running roll film.
Small pillow packs made first, then loaded into a larger bag — for multipacks and club-store formats.
Tell us the shape, the piece weight and the count per pack, and we’ll tell you which of these fits and what it costs to run.
Five ways gummy lines get specified wrong.
None of these show up on a spec sheet. All of them show up in month three.
You buy capacity you can’t use, and you find out after the line is already installed and the room is already the size it is.
Two machines with identical heads can differ by half in output. The tunnel is where that difference lives, and it’s the line item people skim.
The rated output was never for the gummy you actually make. Lock the piece weight before you compare quotes, not after.
Mold lead time then sits on the critical path, and a line that has already arrived at your dock can’t start.
Sticky, irregular product doesn’t behave like a tablet in a counter — and you find out with the whole line waiting behind it.
Four times we'd tell you not to buy this line.
We'd rather lose the quote than lose the installation.
Buying now means buying twice. Lock the formula first — we’ll still be here.
Solve the room before you buy the line, or you’ll own capacity you can’t run.
We don’t build them. We build starch-free depositing lines only, and we’d rather say so now than three emails from now.
Then what you want is a counting and bottling line, not this one.
What your QA gets, in writing.
If you're running under 21 CFR Part 111, your QA has three questions about a new line: can it hold the number, can you prove it held the number, and who signs off that it was installed right.
Deposit weight and active dosing, both under measurement rather than operator judgement.
Every line ships with comprehensive operating manuals, detailed electrical circuit diagrams, and complete 3Q (IQ/OQ/PQ) validation packages to streamline factory commissioning and audits.
Our own engineers travel to your site and commission the line. That is how every line we’ve shipped has been started up.
We build these lines for food and confectionery producers too. The machine doesn’t change; the requirements that apply to you do. Tell us which side you’re on and we’ll match the documentation to it.
What happens after you sign, and after we leave.
3 months
30% deposit upon order, 70% balance prior to shipment.
1-year warranty
Our engineers, at your plant, running your product.
Comes with a starter kit (food-grade seals, O-rings, and nozzles). Built with globally standardized components (Festo, Schneider, Siemens) for easy local sourcing.
U.S. line: +1 (213) 526-8644. That reaches our engineers — not a distributor, not a call centre.
Tell us four things and we'll send back numbers, not a brochure.
Formula base, piece weight, target output, and where you are on drying space. With those we can tell you which line size fits, how much drying floor it needs, and what the back end should look like.
We answer with a line configuration and a real output figure for your piece weight. If the honest answer is that you’re not ready to buy yet, we’ll say that instead.
Prefer to talk it through? +1 (213) 526-8644
