Automatic Gummy Making Machines & Production Lines
Cooking, Depositing, Cooling and Demolding in One Line, 80 to 600 kg/h
For supplement brands moving gummy production in-house. Gelatin, pectin or carrageenan — and we’ll send you a formula if you don’t have one.
Why Choose Our Gummy Making Machines?
Full-Servo Depositing
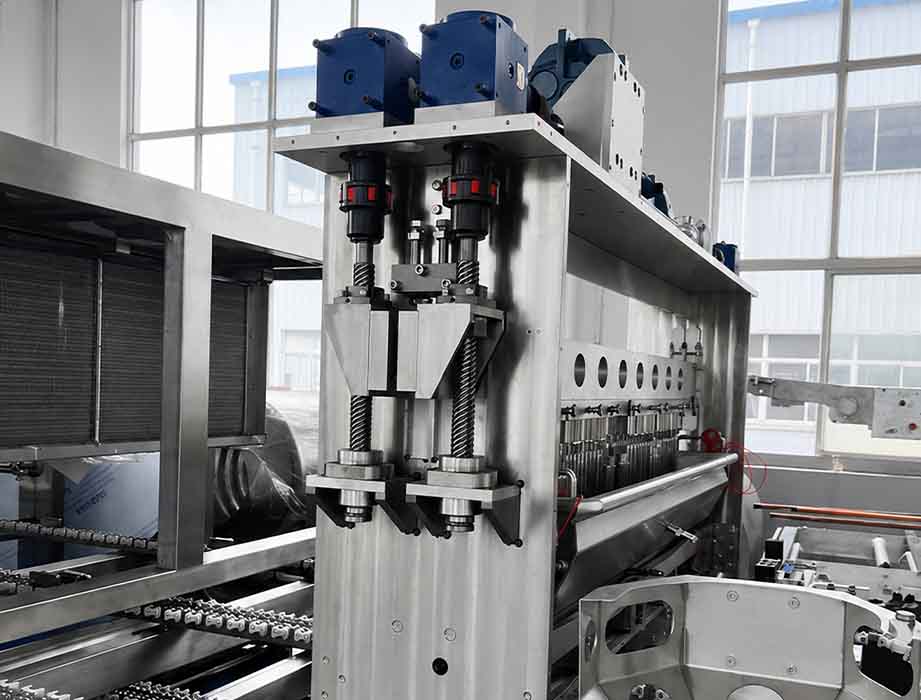
The depositing pistons run on servo motors with solid screw rods and linear guides. Chain-driven depositors are the common alternative — the chain stretches, and fill weight drifts after a few months. That’s a difference you see in your weight checks a year in, not on day one.
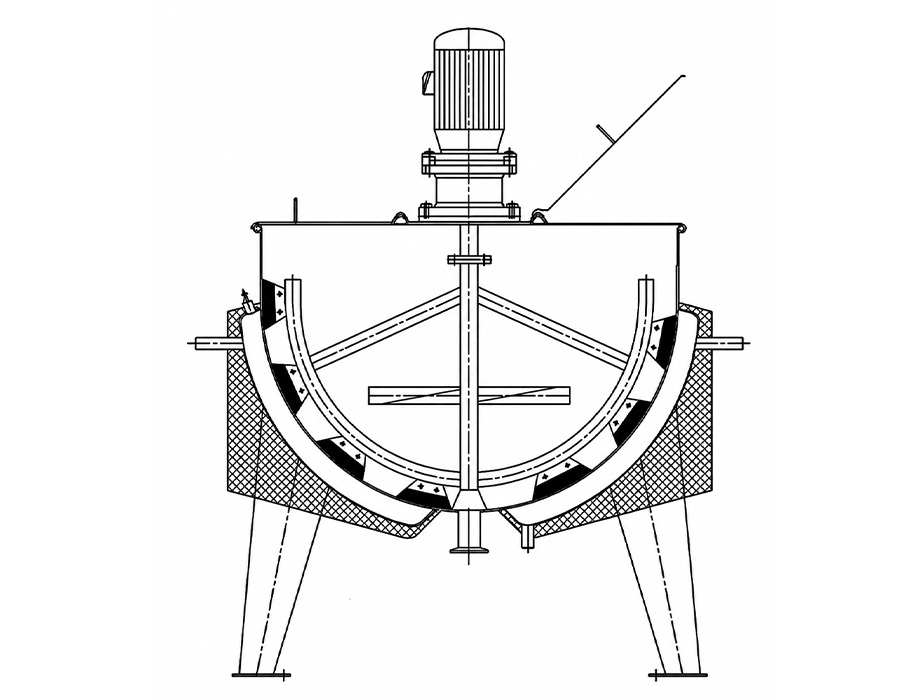
Three-Layer Jacketed Cooker
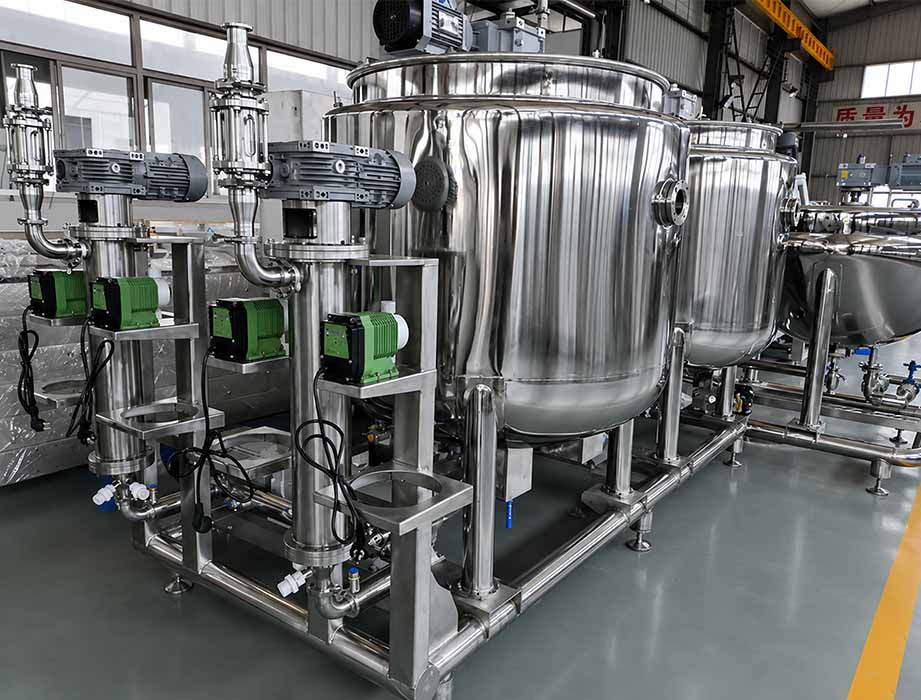
200 litres working volume, electric or steam heating. Three walls: the middle packed with insulation, the outer one cool enough that an operator brushing past it doesn’t get burnt. Scraping side stirring, an internal thermometer, and a CIP ball that connects to your cleaning system.
Lobe Transfer Pumps
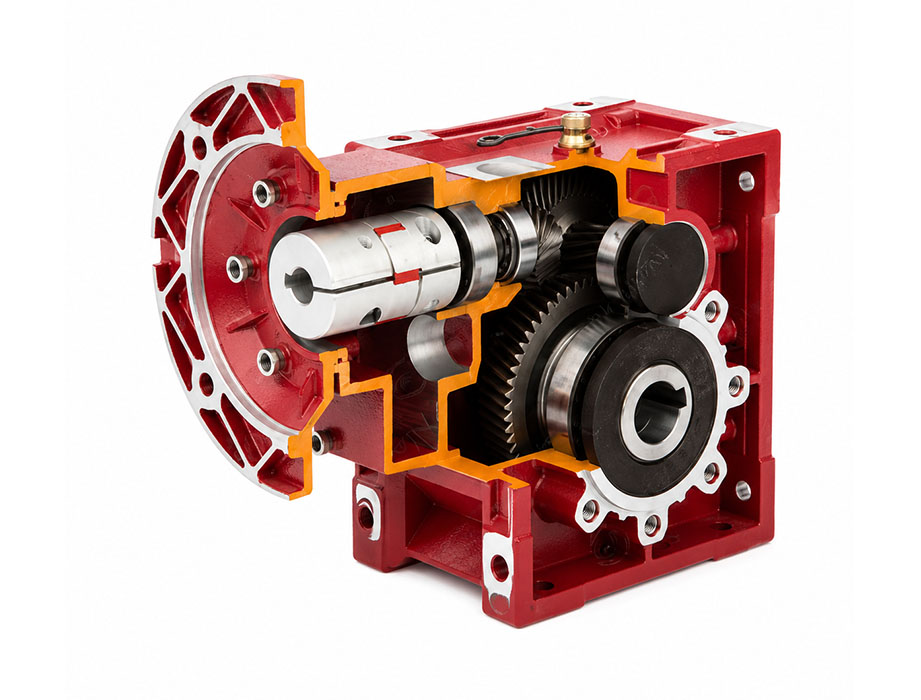
Syrup moves between the cooker, the storage tank and the depositor on lobe pumps rather than gear pumps. Two rotors turning against each other carry the syrup through in separate pockets — gentler on the product, steadier flow, and a longer service life than a gear pump under the same duty.
Vertical Dynamic Mixing
Flavour, colour and actives are blended in a vertical mixer rather than a horizontal one. Horizontal mixing lets dense material — mineral powders, botanical extracts, organic acids — settle at the bottom of the pipeline. The vertical design forces the mass upward, and there’s a window so the operator can see it.
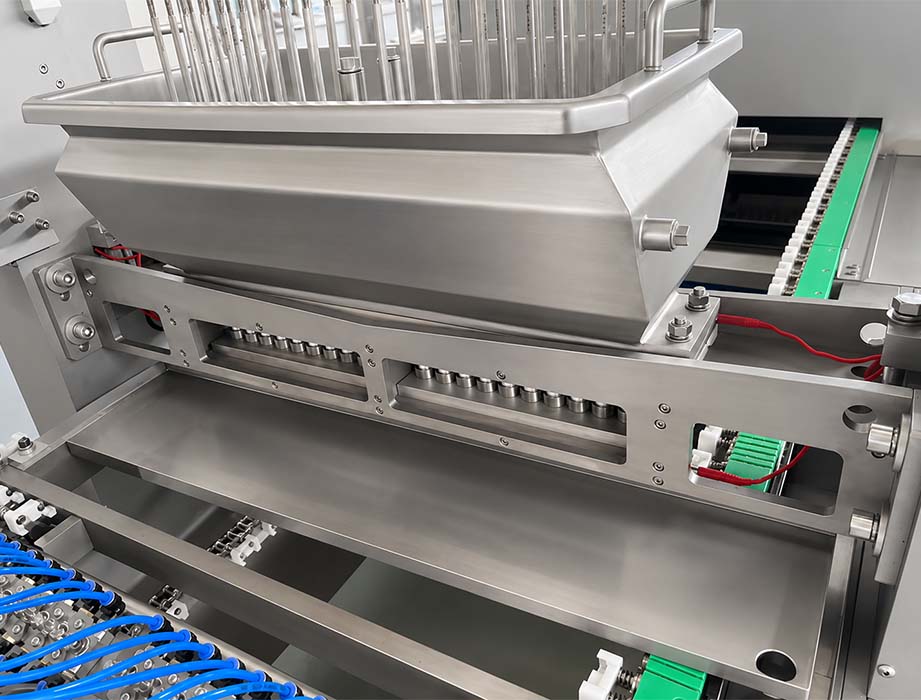
Anti-Scald Hopper
The depositing hopper is shaped and guarded so operators working at the head aren’t exposed to the hot surface. All welds inside the hopper are polished — no dead corners where syrup can sit.
Suspended PU Belt
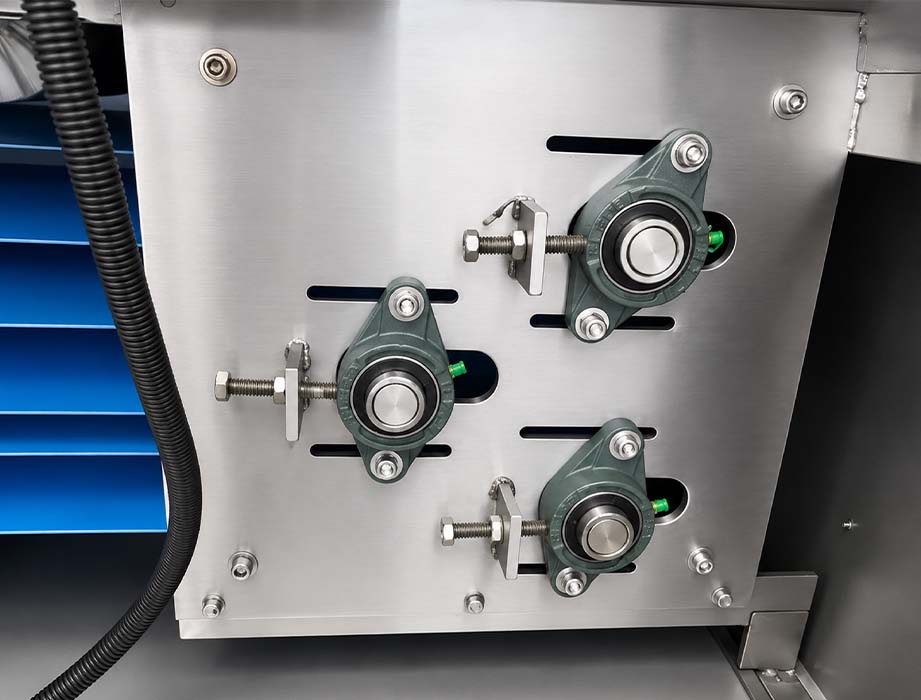
The blue PU belt runs suspended off the tunnel floor with a pneumatic cylinder holding tension automatically. Belts that sit flush against the tunnel trap spilled syrup underneath — they glue down and they’re hard to clean. Mechanical tensioners wear the belt out faster.
Industry Applications
Four Line Sizes
Model | Output | Depositing speed | Steam | Power | Length | Weight |
APK-GM80Q | 80 kg/h | 25–35/min | 80 kg/h, 0.4–0.6 MPa | 55 kW | 8 m | 2,500 kg |
APK-GM150Q | 150 kg/h | 25–45/min | 250 kg/h, 0.5–0.8 MPa | 65 kW | 16 m | 3,500 kg |
APK-GM300Q | 300 kg/h | 25–45/min | 300 kg/h, 0.8–1.2 MPa | 75 kW | 18 m | 4,000 kg |
APK-GM600Q | 600 kg/h | 25–45/min | 500 kg/h, 1.6–1.8 MPa | 85 kW | 20 m | 5,000 kg |
All four run the same servo depositing, the same full-plate demolding and the same mold system. What changes is throughput — and what that costs you in steam, power and floor.
Two things worth noting before you choose on output alone. Steam pressure climbs steeply: the GM600Q needs 1.6–1.8 MPa against 0.4–0.6 for the GM80Q, and that boiler requirement stops more buyers than floor space does. And the GM600Q is only 2 metres longer than the GM300Q for twice the output.
Product Range Overview
Four lines, from the size most brands start with to the largest we build.
What Your Plant Needs to Supply
Utilities
Steam — 80 to 500 kg/h depending on line size, at 0.4 to 1.8 MPa. Compressed air at 0.2 to 0.3 m³/min. Electricity, water inlet and drainage.
Air handling
Two dehumidifiers — one for the cooling area, one for the packing room. Two air conditioners, same two rooms.
Room conditions
Forming area: 25–30 °C, humidity 45% or below. Cooling tunnel: 5–10 °C. Drying room for pectin: 25–30 °C, humidity 25–45%.
Floor and people
8 to 20 metres of line length depending on size, plus working clearance. Two to three operators — that number is the same on every line we build, so a smaller machine doesn't save you headcount.
What we supply
The line, a layout drawing against your actual room and the formula if you don't have one. Installation and operator training are a paid service, quoted in your proposal.
Two things worth raising early. Steam is the one most buyers overlook: if you don’t have a boiler, tell us and we’ll quote the electric heating option instead. And no machine fixes a room that swings — if you can’t hold the forming conditions yet, say so before you order rather than at commissioning.
That’s not a problem, and it’s not a reason to wait. We’ll send you production formulas for both gelatin and pectin — ingredient ratios and process steps — free, whether you buy from us or not.
Documentation & Selection Support
Verify our quality standards and simplify your procurement process with our official documentation.
Product Portfolio Catalog
CE Declaration of Conformity
Gelatin and pectin formulas
Gummy Making Machine Technical FAQ
Moisture stabilization varies heavily based on the hydrocolloid or stabilizer base material used. Once candies exit our full-plate pneumatic demolder, they must enter a dedicated drying environment with these precise bounds: (a) Gelatin base: Temp 22-25℃, Humidity <40%, Curing time: 8-12 hours; (b) Pectin base: Temp 25-30℃, Humidity 25-45%, Curing time: 20-24 hours; (c) Carrageenan base: Temp 35-40℃, Humidity <16%, Curing time: 12-15 hours.
Cooking is the slowest step on a gummy line. The cookers and a syrup storage tank sit on one frame and work in turns: one cooker dissolves the next batch while the storage tank feeds the depositor. The depositor keeps running while the next batch cooks.
Standard horizontal blending bars suffer from natural gravity drop, causing dense mineral powders, functional botanical extracts, or organic acids to pool at the base of the pipeline, which ruins dosage uniformity. Our advanced Vertical Dynamic Flavor and Colors Mixer forces the processing mass upward into a high-shear fluid vortex. This active mixing pattern keeps dense actives in suspension through the run concentration uniformity, and operators can monitor fluid consistency in real time through the built-in visible window.
Traditional configurations mount the driving motor at the front depositing filling station, which pulls the heavy mold carrying chain from the front. Over long schedules, this mechanical setup causes minor chain links to stretch or twist, which directly ruins the tracking precision at the filling station. AIPAK moves this component to a postposition motor layout inside the cooling tunnel exit area. Pulling the chain from the far end keeps it level and evenly tensioned, so the molds stay lined up under the depositing nozzles.
High-capacity commercial runs emit heavy hot syrup vapor that naturally turns into thick ice frost across standard short cooling tunnel coils, reducing air circulation and spiking humidity levels inside the chamber. Our customized, extended Air Handling Unit (AHU) incorporates specialized de-frost heating elements. This system regularly clears moisture accumulation, keeping the inner tunnel humidity significantly lower than normal tunnels to prevent the soft candies from sweating or melting on the belt.
Flat conveyor belts that run flush against the inner metal base of the tunnel track trap spilled syrup underneath, which glues the belt tightly to the floor and burns out drive motors. Our advanced blue non-stick PU belt uses a suspended design backed by an active pneumatic cylinder tensioning device. Nothing gets trapped under the belt, the belt lasts longer, and air knives keep pieces moving cleanly off the belt.
Yes. The control panel is a fully enclosed stainless steel cabinet, and every power, sensor and heater connection uses a separate water-resistant plug. Your cleaning crew can spray down the frame and the inside of the cooling tunnel.
Every terminal, air connection and part on the line carries an ID mark, so you can tell us exactly which part you need. A kit of wear parts ships with your line. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
Yes, free. We’ll send you production formulas for both gelatin and pectin, with ingredient ratios and the process steps. You don’t have to buy from us to have them.
The cooker can be built with electric heating instead. Tell us at enquiry rather than after the quote — it changes the build and the price, and it’s much easier to specify than to retrofit.
Yes. Our machines are certified and use certified electrical components. Because the exact scope depends on the model and electrical configuration you select, our factory confirms it in writing before production.
Not sure which line size?
Tell us your target output in kg per hour and your piece weight. We'll tell you which one, and why.
Send us your formula — or ask us for one
If you have a formula we'll tell you what the line needs to run it. If you don't, we'll send you ours. Free, either way.
Send your floor dimensions
Length, width, height, and where the doors and columns are. We'll draw your line against your actual room.
Reply within one business day. Formulas sent free, whether you buy or not.