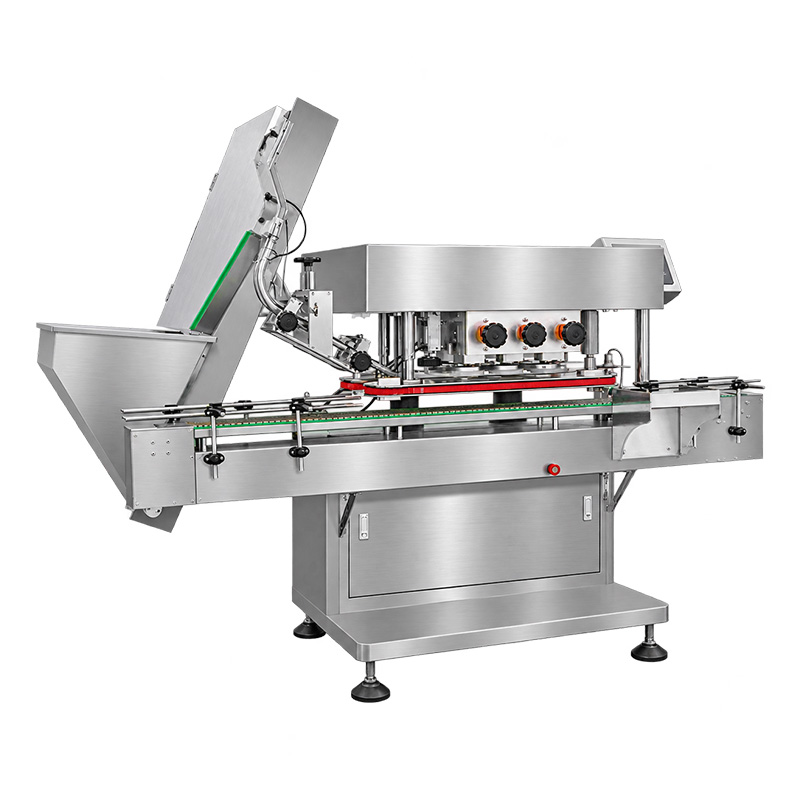
Home » APC-D901 Press-Screw Capper
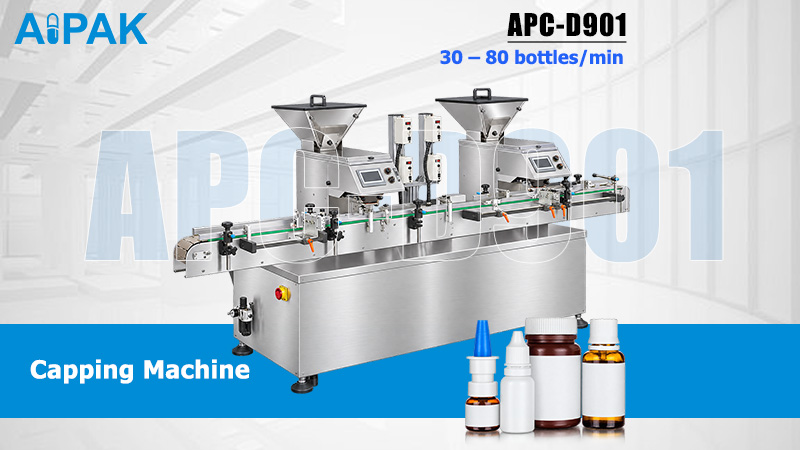
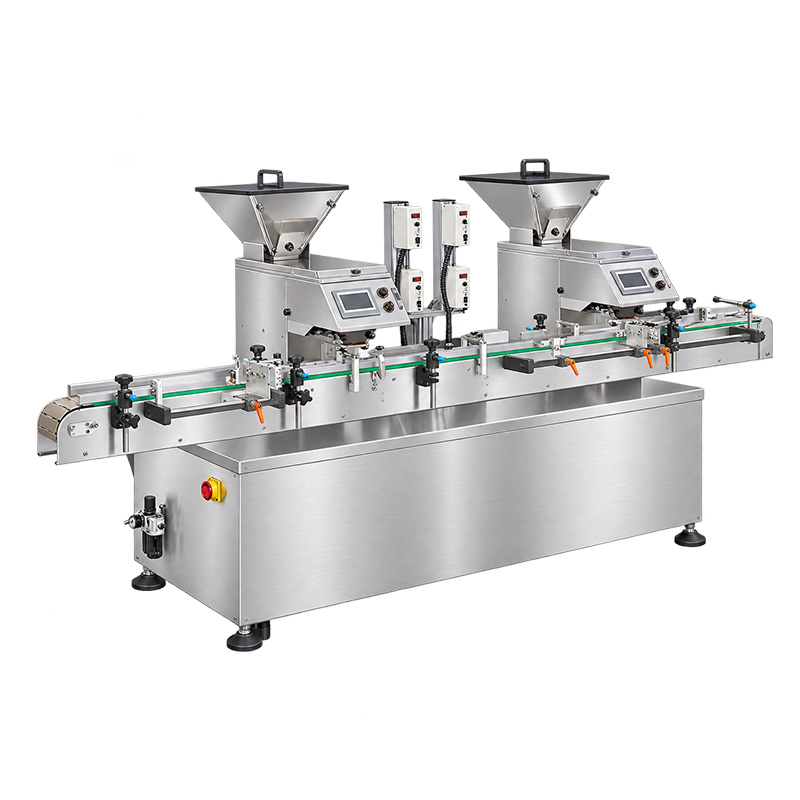
APC-D901 Press-Screw Capper
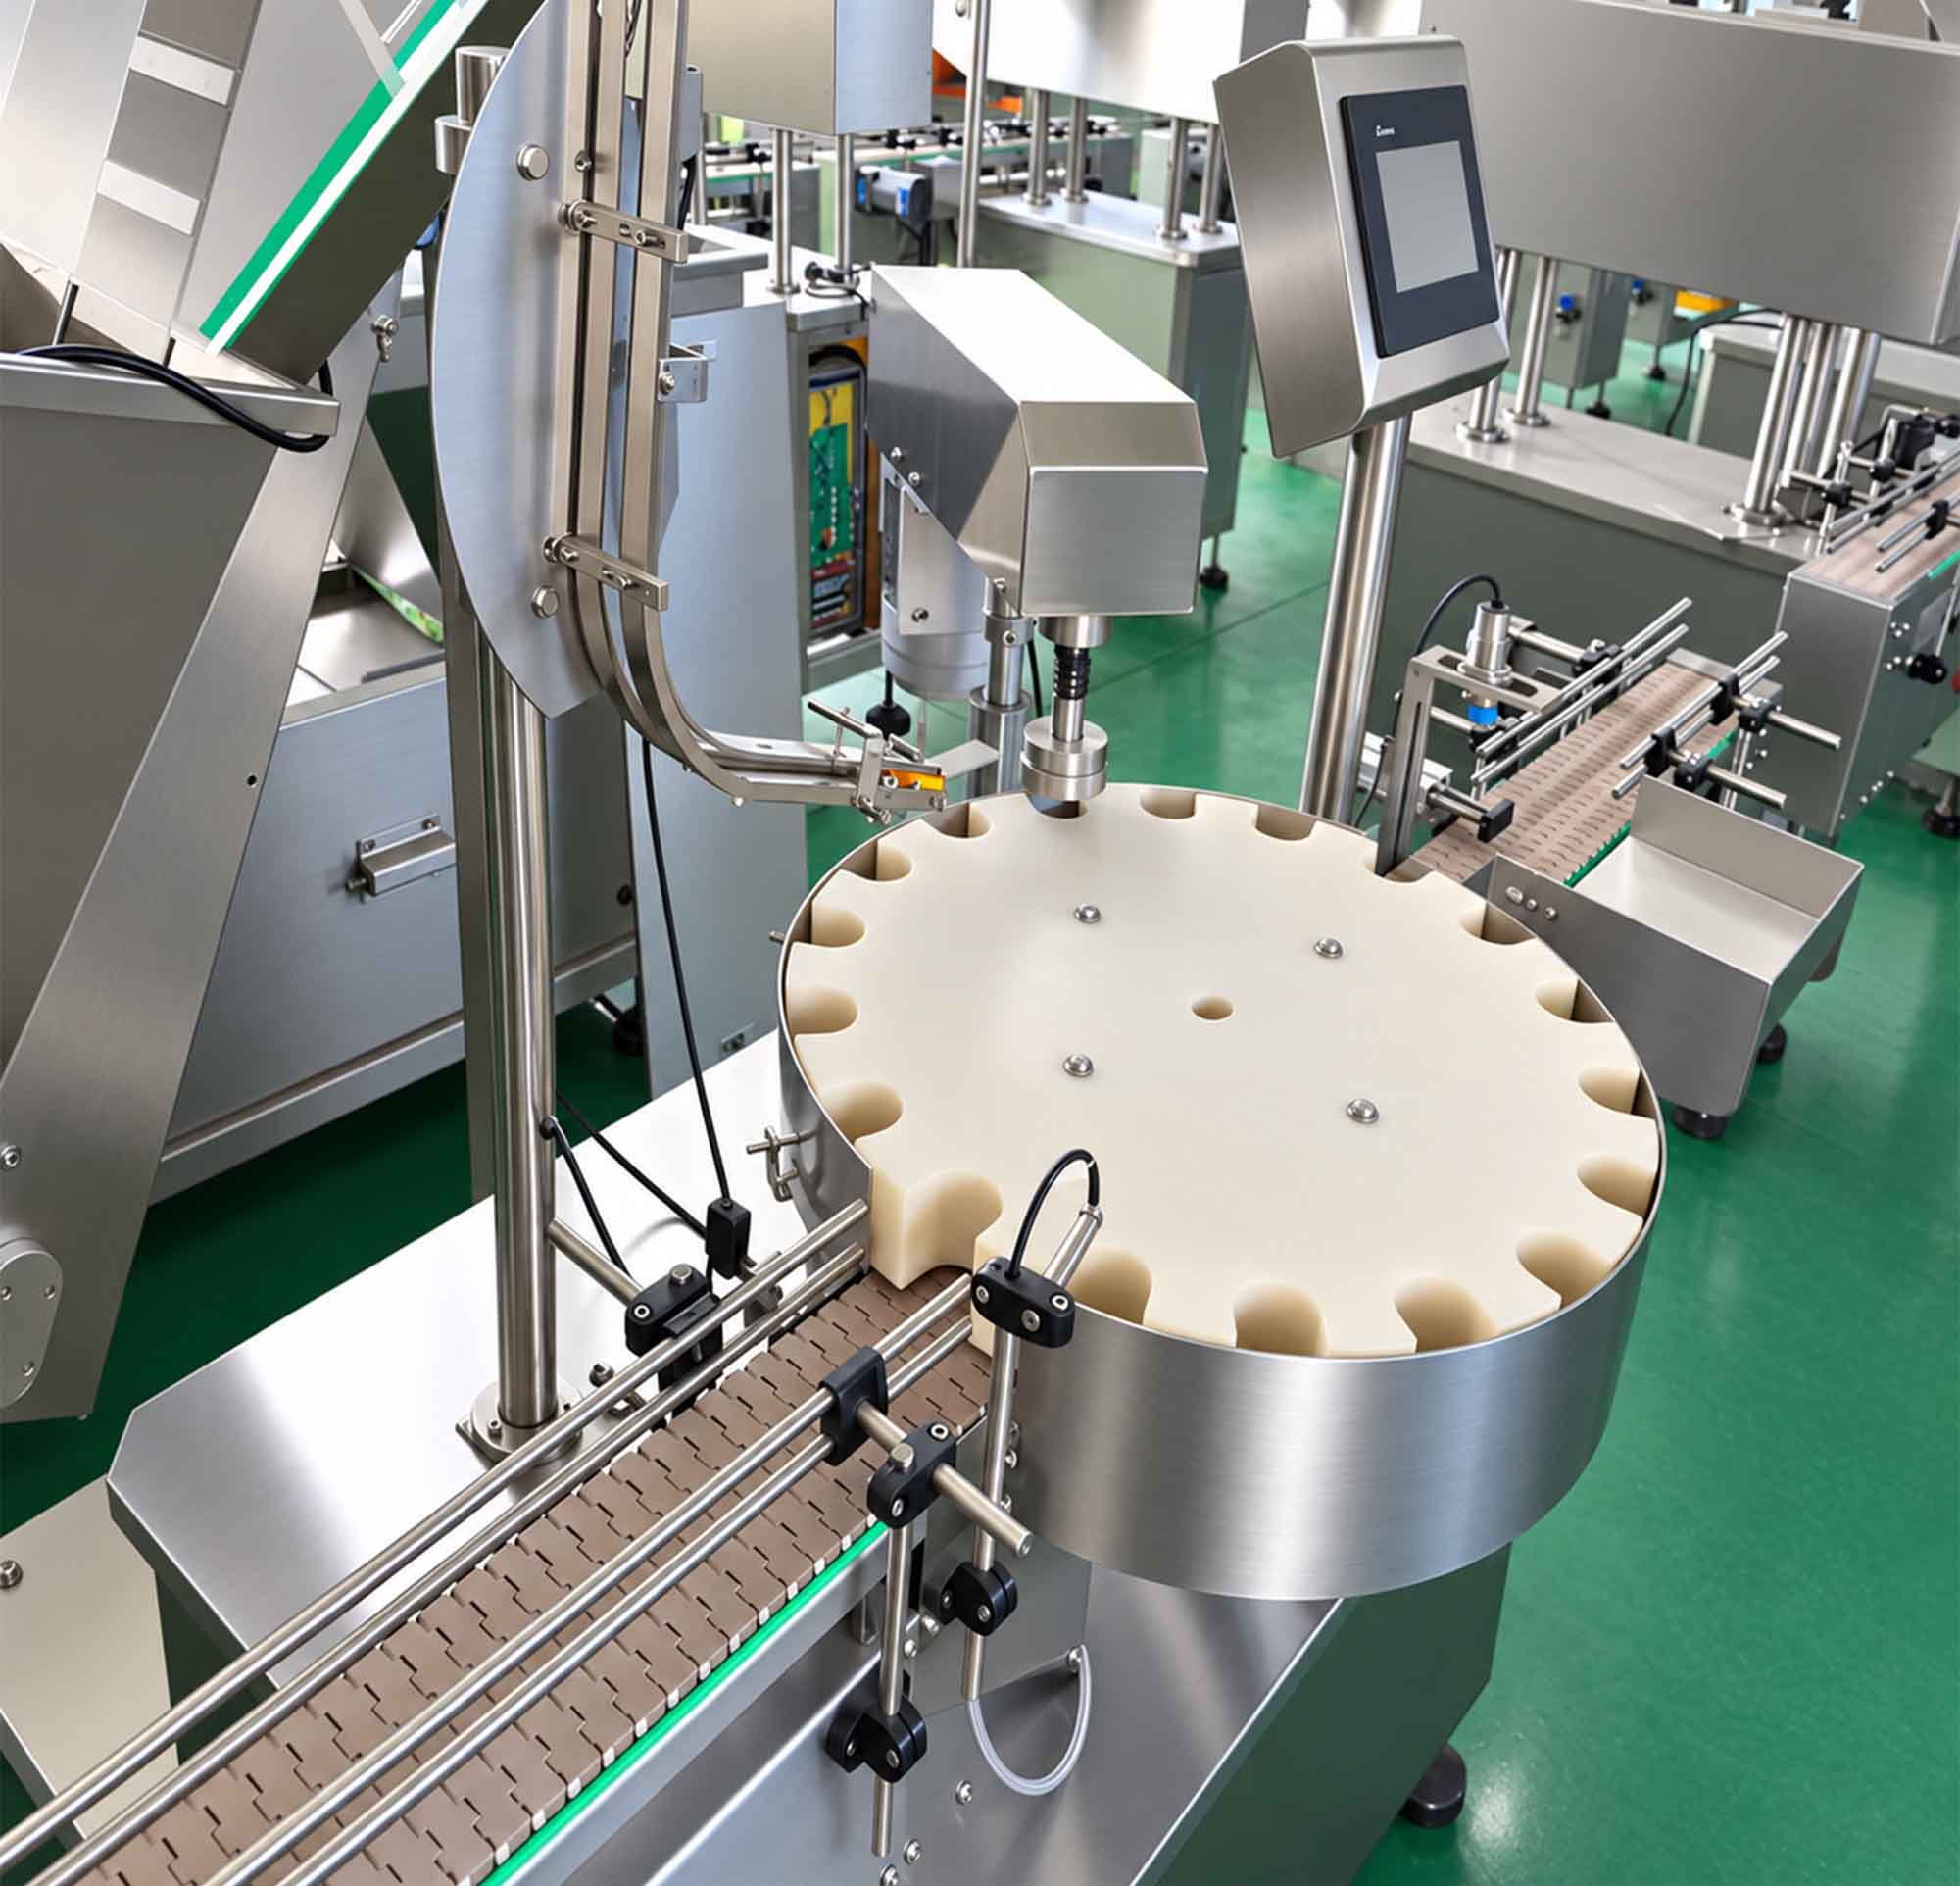
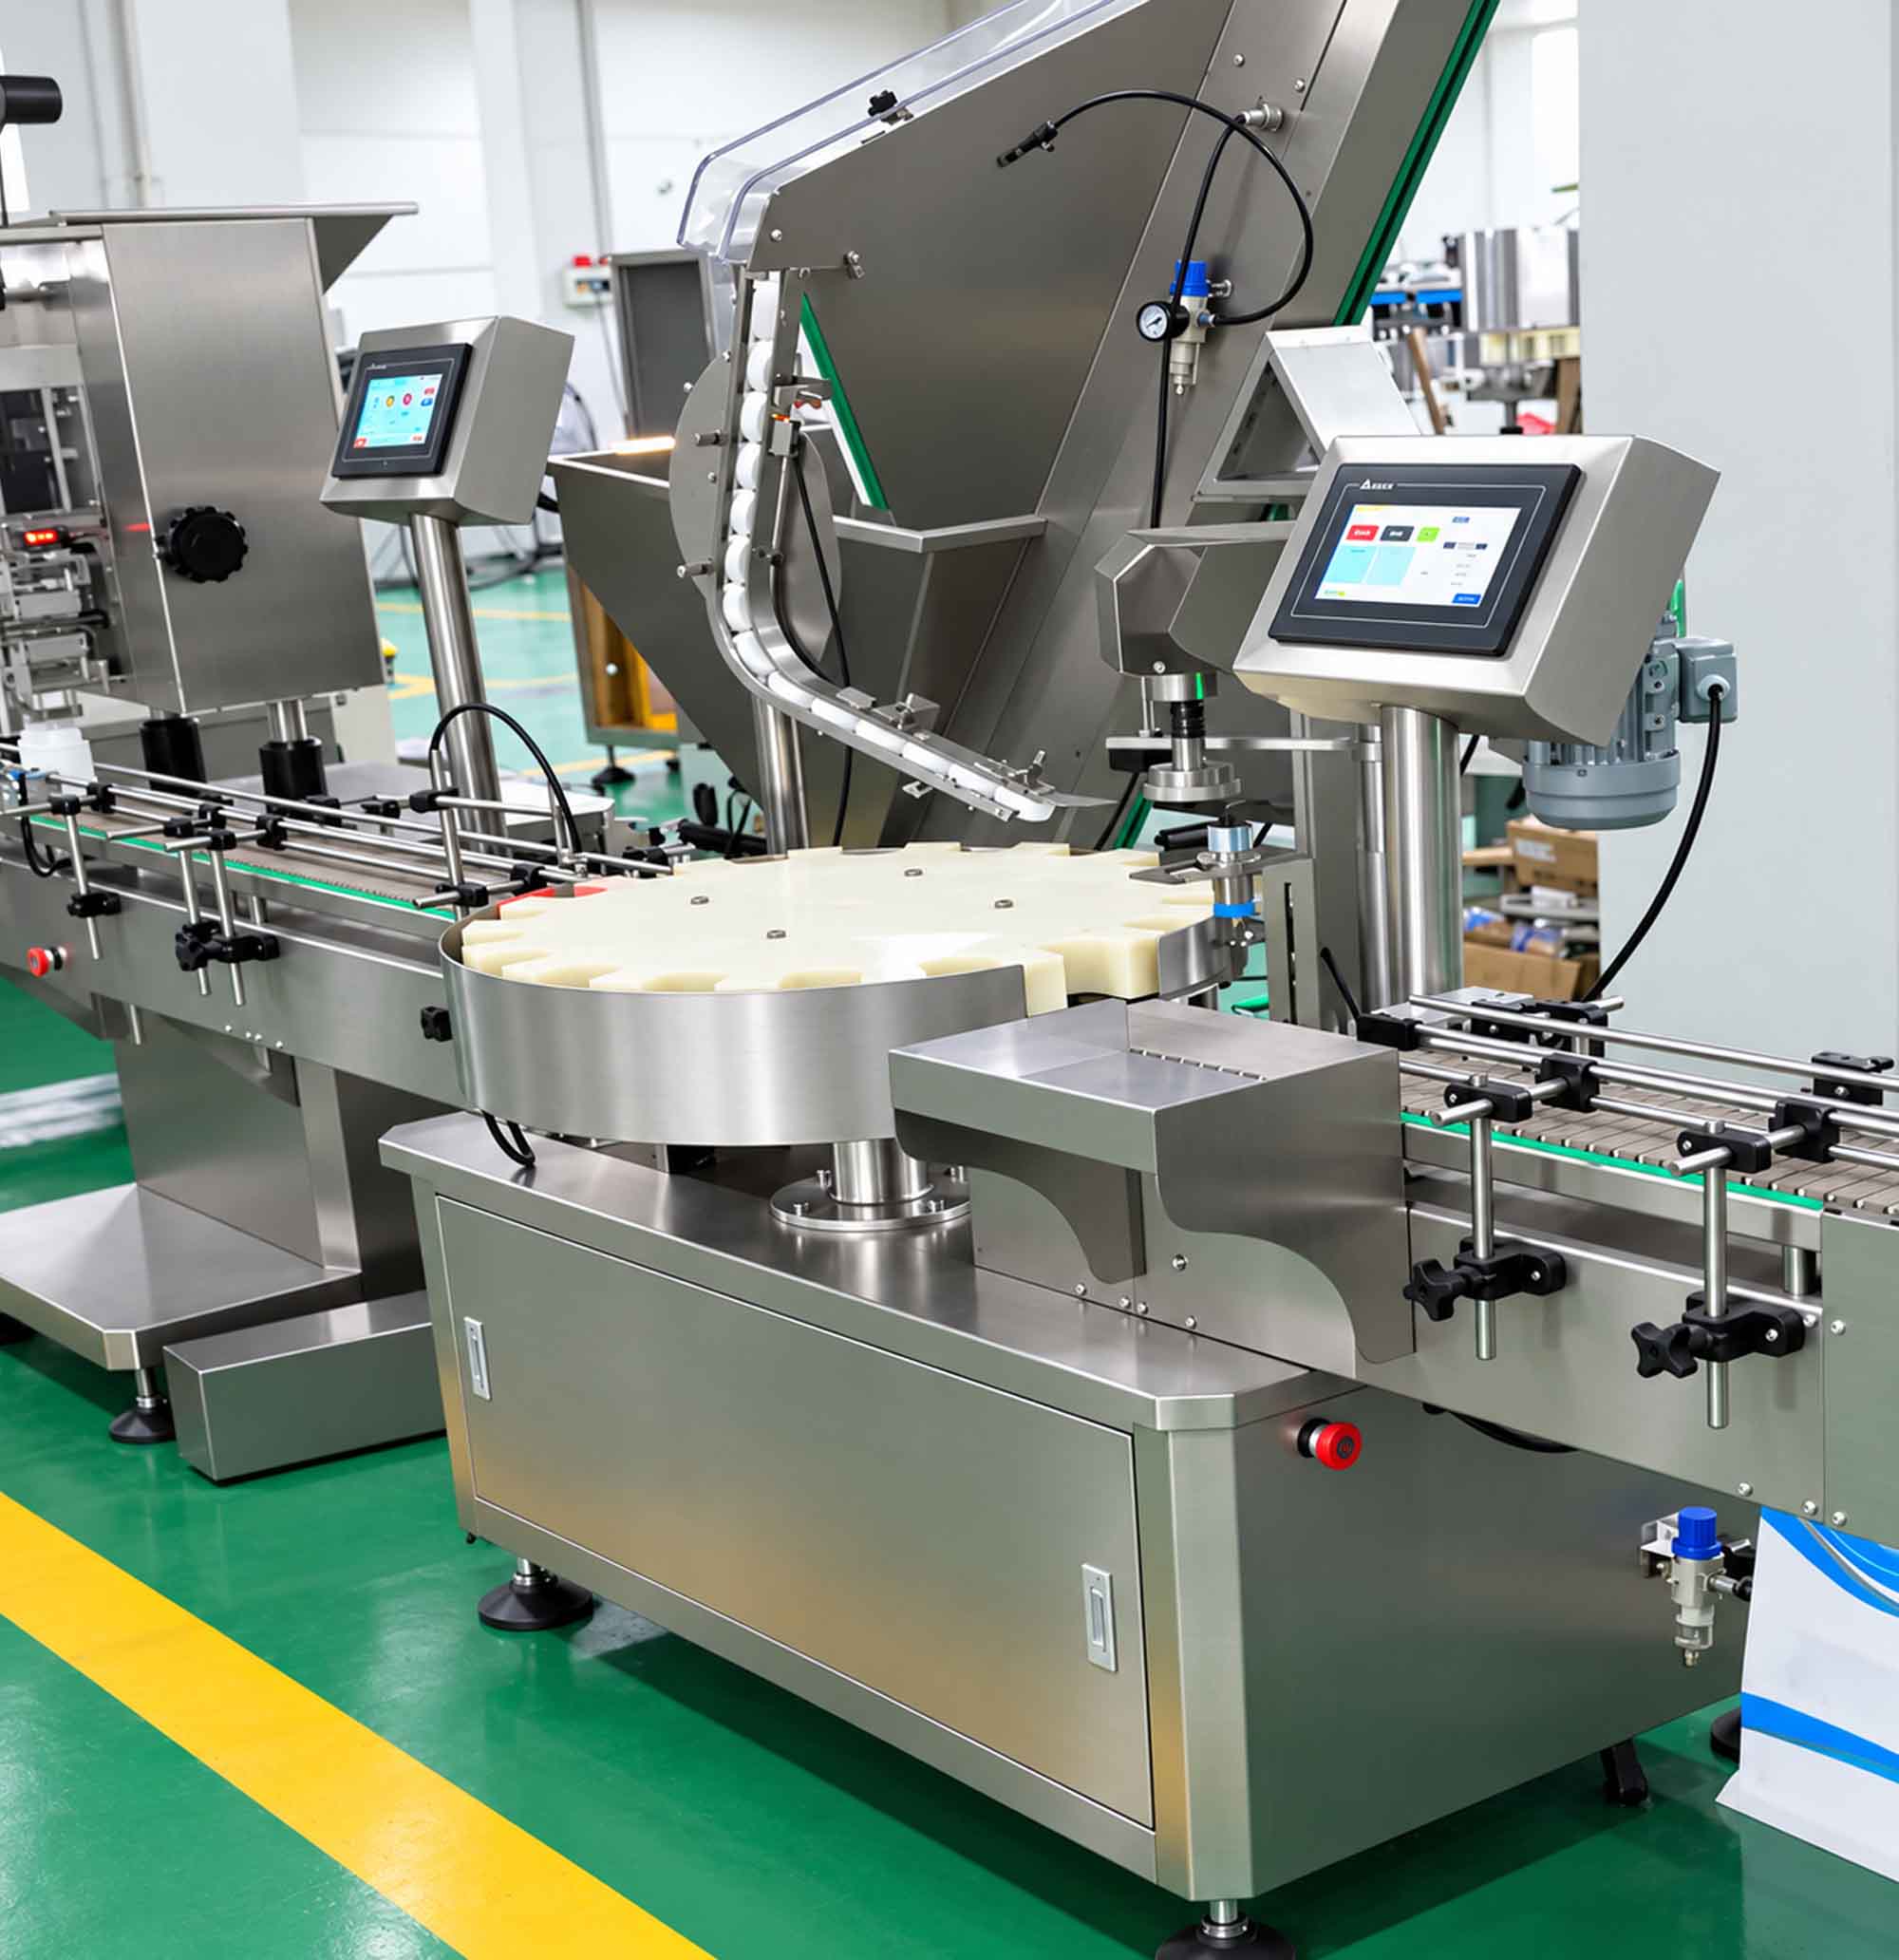
The APC-D901 presses and screws in one station, at 30 to 80 bottles per minute. It was built for the containers that give ordinary cappers trouble — shaped bottles, flat bottles, anything that won’t sit still under a capping head. If your bottle isn’t a plain cylinder, start here.
- Press and screw in one station— handles closures that need both actions
- Built for shaped containers— the positioning arrangement is the point of this machine
- 30 to 80 bottles per minute— steady rather than fast, because odd shapes take longer to hold
Direct from our factory | Lead time confirmed in your quote | Installation and training available | Spare parts listed in your quote
Is the APC-D901 the right capper for you?
✓ This is a fit if…
- Your bottles are shaped, flat or oval rather than plain round
- Your closure needs pressing and screwing — the cap seats down before it turns
- Your line runs up to 80 bottles per minute
- You've had positioning problems with a standard capper on these containers
- You run standard, tamper-band, double-layer or flip-top plastic caps
✕ Look elsewhere if…
- Your bottles are standard round and your caps just screw on → the APC-D902 runs faster, up to 120 per minute, for less
- Your caps only press on → the APC-D904 is the press machine, and it's smaller and simpler
- Your line runs faster than 80 bottles per minute → shaped containers slow a line down. If you need more, tell us the bottle and we'll say what's possible
- You need crooked-cap or missing-liner rejection → that detection is on the APC-D902. This machine stops for a missing bottle or missing cap, but doesn't reject a cap that went on badly
- You're capping glass → talk to us first about the handling arrangement
Technical specification
| Parameter | Value | What this means for you |
| Capping speed | 30 – 80 bottles / min | Slower than a round-bottle capper, because shaped bottles need holding |
| Capping method | Press and screw combined | The cap seats down, then turns |
| Cap types | Standard, tamper-band, double-layer, flip-top plastic caps | |
| Container shapes | Round and shaped containers | The positioning arrangement is built for the awkward ones |
| Bottle size range | Φ20 – Φ120 mm / Height: 50 – 300 mm | Send us your bottle — shape matters more than size here |
| Cap diameter range | Φ15 – Φ65 mm | |
| Torque | Adjustable, 0.5 – 4.0 N·m | Set tight enough to hold a foil liner, loose enough to open |
| Detection | No bottle / no cap, with self-diagnosis | Stops on a missing bottle or cap. Does not reject a badly applied cap |
| Power | 1.5 kW, 60 Hz | Built to your U.S. supply. We confirm the voltage with your quote |
| Compressed air | 0.6 MPa, 0.3 m³/h | Small demand — most existing compressors cover it |
| Machine dimensions | 2150 × 1050 × 1900 mm | |
| Machine weight | 600 kg |
Model comparison
Model | Speed | Method | Best for… |
|
APC-D901 | 30–80 btl/min | Press and screw | Shaped, flat or oval containers that are hard to hold | You are here |
APC-D902 | 50–120 btl/min | Screw, friction wheels | Standard round bottles at line speed | |
APC-D903 | 60–180 btl/min | Screw, high speed | High-speed lines above 120 bottles per minute | |
APC-D904 | 40–120 btl/min | Press only | Caps that push on rather than screw on |
Your closure and your bottle shape decide this, not your line speed. A press-on cap on a screw capper and a screw cap on a press capper both come out damaged.
Press and screw in one action
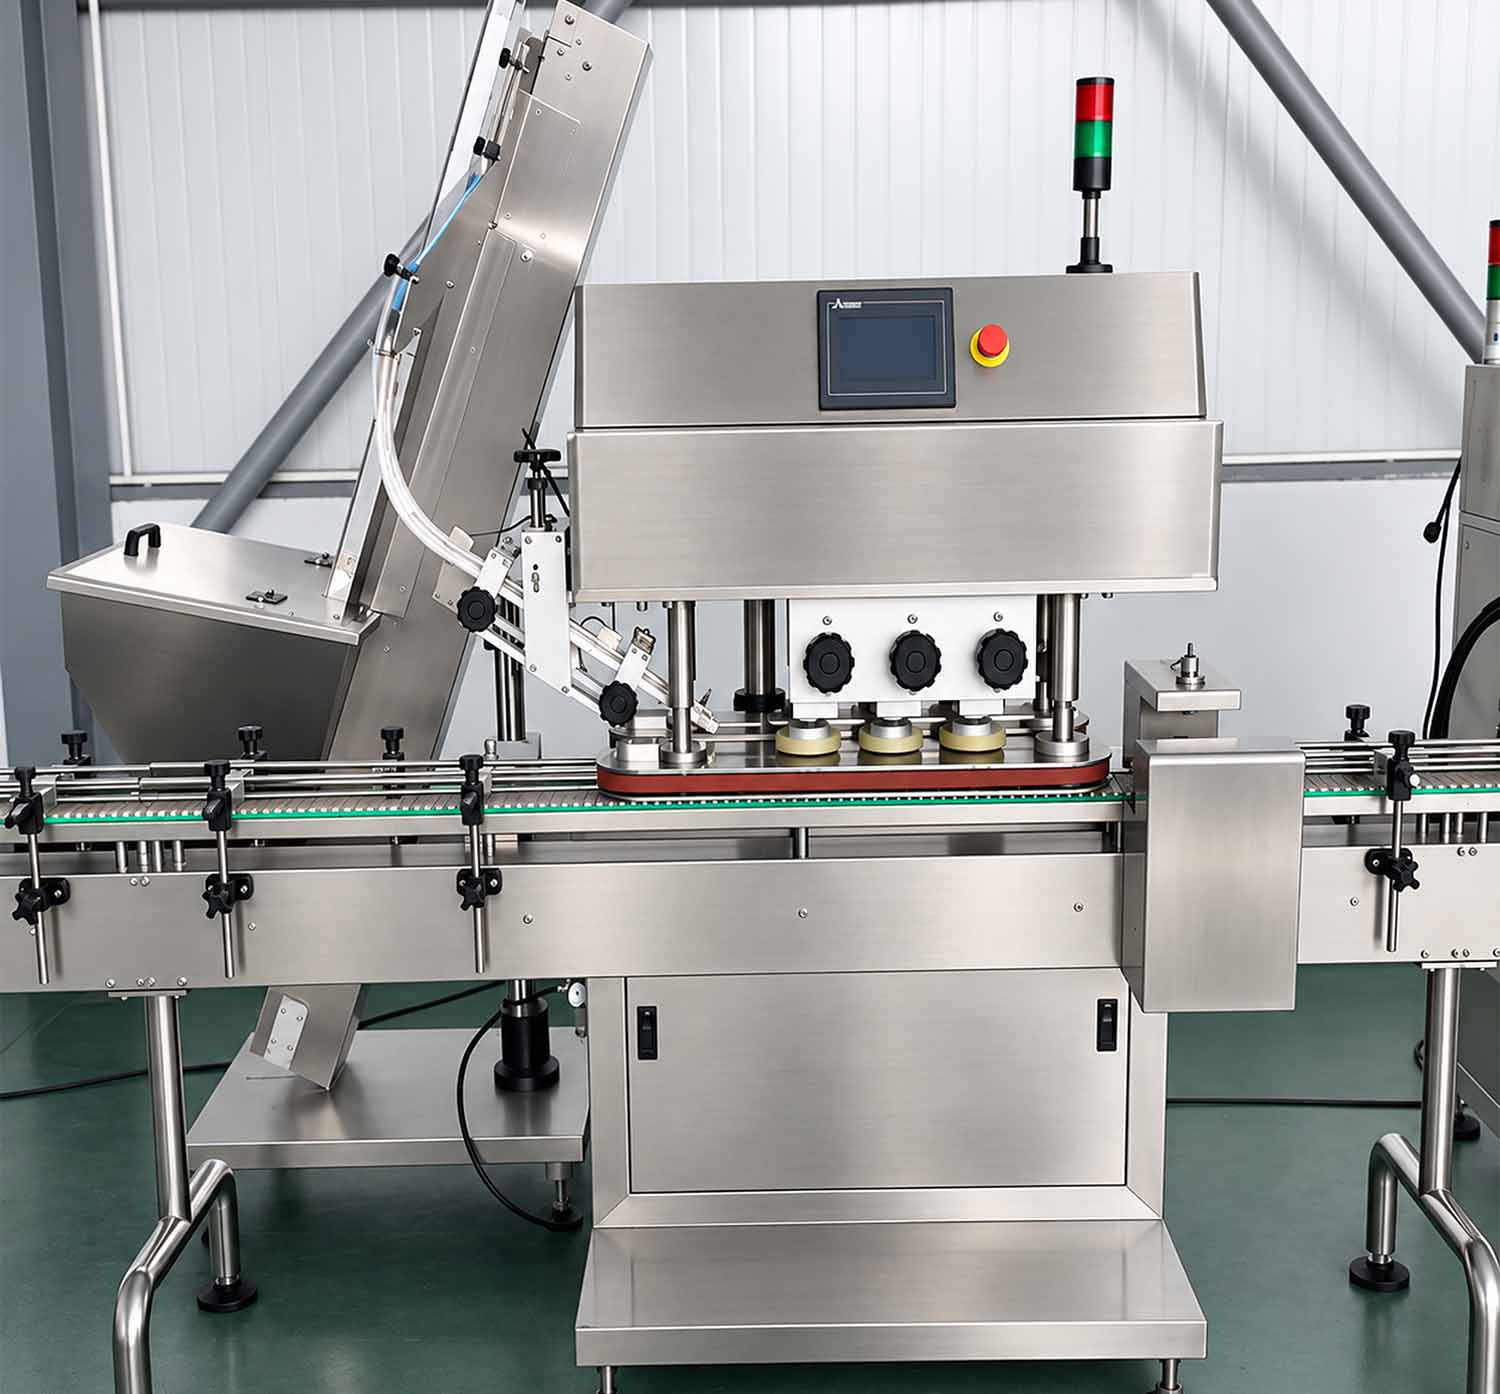
The head seats the cap down before turning it. For closures that need both — a cap that has to be pushed onto the neck before the thread engages — doing it in one station avoids the alignment loss that comes from splitting the job across two.
Torque is adjustable. Set it tight enough that the foil liner presses against the bottle land, loose enough that your customer can open the bottle. That single setting decides both problems.
Positioning for shaped containers
A round bottle finds its own center under a capping head. A flat or oval bottle doesn’t — it can rotate, tilt, or sit off-center, and a cap applied to a bottle in the wrong position goes on crooked.
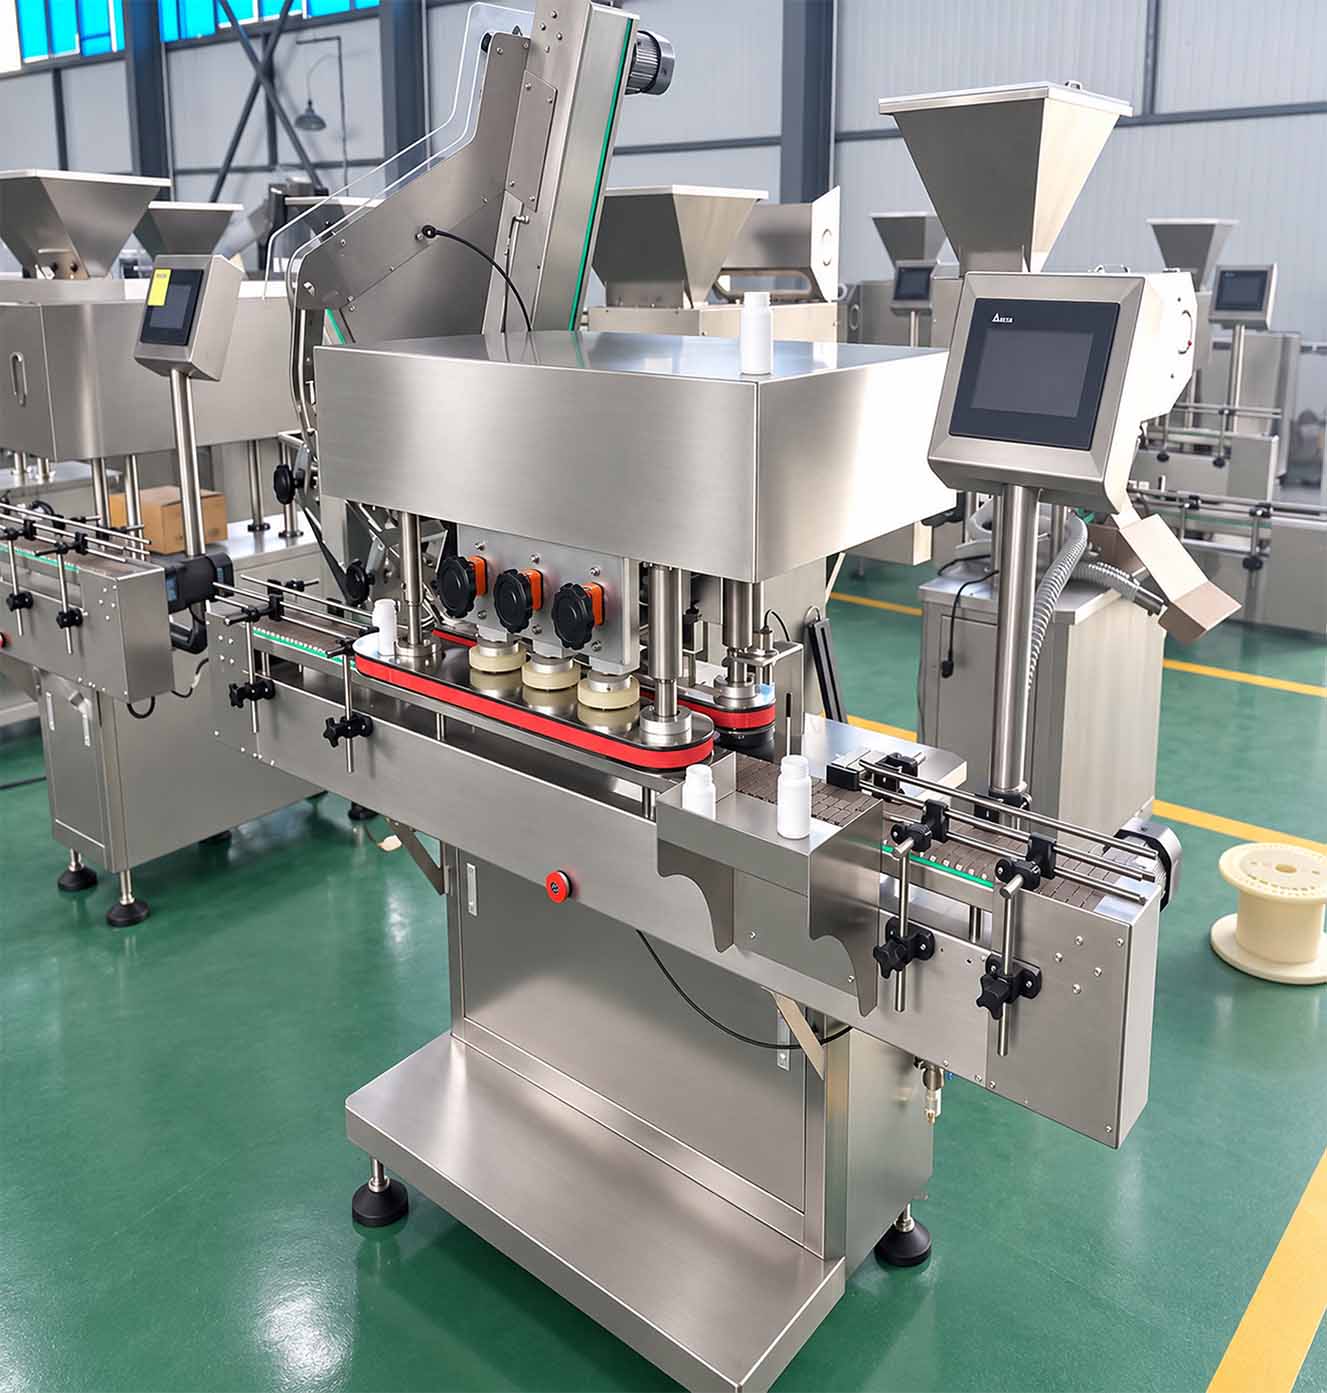
The positioning arrangement on this machine holds the container in a fixed orientation through the capping stroke. That’s the whole reason to buy this model rather than a faster one.
Tell us your bottle shape at the quotation stage. The holding arrangement is configured to it before the machine ships.
Stepped cap elevator
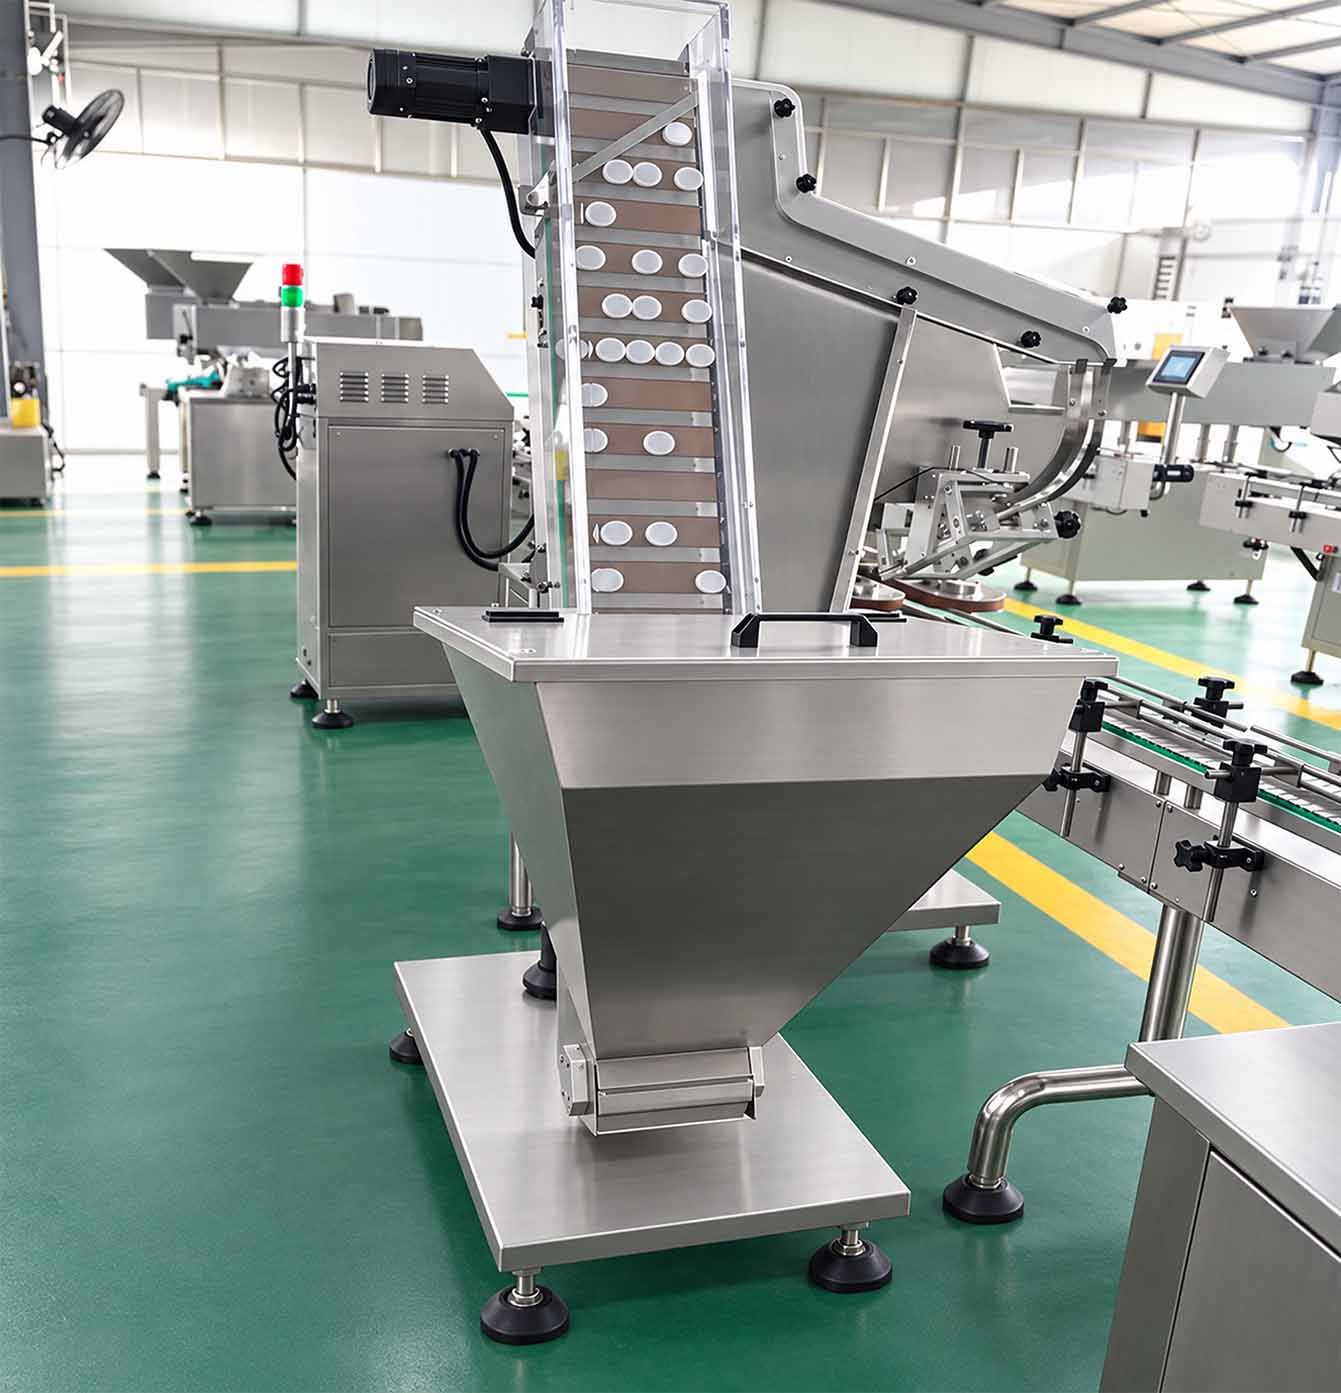
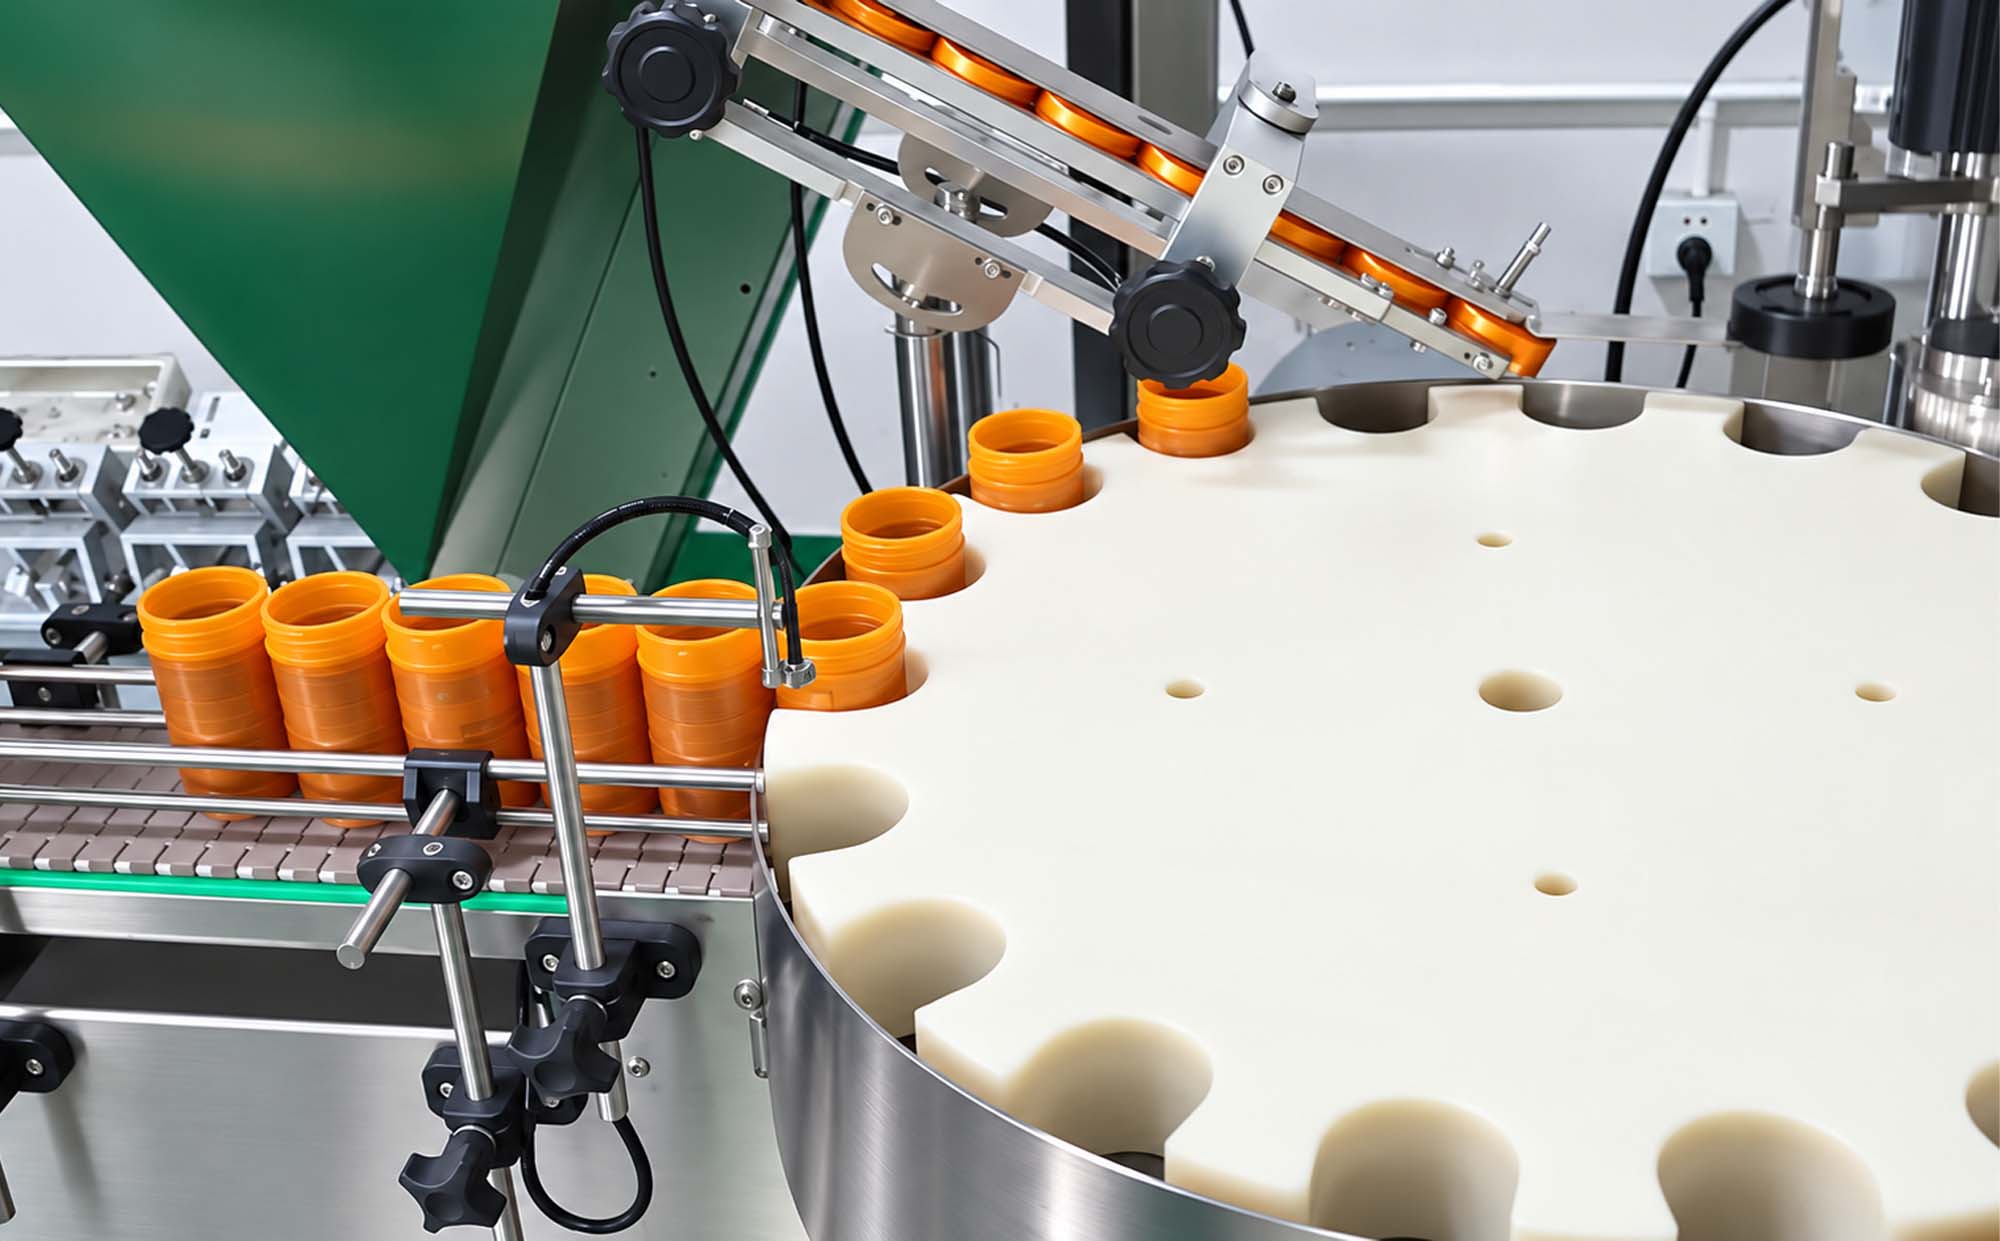
Caps are lifted by a stepped elevator rather than a vibratory bowl. It runs quieter and cap delivery stays steady rather than surging.
Caps that arrive facing the wrong way drop back into the hopper instead of being fed to the bottle. That’s what stops a wrong-way cap becoming a jam.
Ideal Applications & Industries
Flat and oval supplement bottles
Flat bottles look good on a shelf and are difficult to cap. They rotate under the head unless something holds them. If you’ve been capping these by hand because the machine kept applying caps crooked, this is the reason why.
Closures that seat before they turn
Some tamper-band and double-layer caps have to be pushed down onto the neck before the thread catches. Screwing without pressing first cross-threads them.
Oval tincture and dropper bottles
A 30 ml oval bottle rotates under a capping head unless something holds it. Dropper caps make it worse — the pipette adds weight off-centre. This is the container that sends people back to hand-capping.
What changing over involves
What you changed | What gets adjusted | Roughly how long |
Same bottle, different cap color | Nothing | 0 |
Different cap diameter | Cap chute and capping head | 15–30 minutes |
Different bottle height | Head height, conveyor guides | 15–30 minutes |
Different bottle shape | Positioning arrangement, guides, torque check | 15–30 minutes |
Shape changes take longest. Height and diameter are adjustments. Changing from a round bottle to a flat one means resetting how the container is held, which is the slowest changeover on this machine.
Re-check torque after every changeover. It’s the one setting you can’t judge by looking at the bottle. Cap a few, check them, then run.
Write down the holding setup for each container. Together with torque and head height, that’s your changeover sheet. A repeat job takes a fraction of the first setup.
Three things to check before you buy any capper
Torque, and whether it holds
Ask any supplier what torque range their machine covers and how it's verified. Then ask what happens to that setting over a full shift. We run your bottles with your caps at factory acceptance testing and give you the torque readings, not just a demo.
The manual
Your operator sets torque, head height and the container holding arrangement. They need to know what an under-torqued cap looks like before it reaches the sealer. Ask to see the English manual with the settings procedure in it.
Installation and training
The machine runs out of the crate. Getting a shaped bottle to hold squarely takes someone who's done it before. Our engineers install it, set it up for each of your containers, and train your operators.
Why Choose AIPAK?
One Point of Contact
One project engineer handles your machine from proposal to commissioning, so you’re not chasing five suppliers for one answer.
We Run Your Bottle and Cap Before You Order
Send us your bottles and caps. We cap them on the machine and send you the video and the readings. You decide whether to talk quotes after that.
A U.S. Number, Answered by Us
+1 (213) 526-8644, answered by our engineers 9 AM–7 PM China time, Monday to Friday. That’s evening and overnight in the U.S., so leave a message or send a WhatsApp anytime and we’ll pick it up first thing.
Spare Parts and Lead Time, in Writing
A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
Deep Dive FAQ
It depends on your container shapes, cap sizes and line speed. Send us a bottle and a cap and we’ll reply within one business day. Most quotes include a layout showing where it fits.
Two reasons. Your closure may need seating before the thread engages, or your bottle may be shaped in a way that a standard capper can’t hold squarely. If neither applies, the APC-D902 is faster and costs less.
Torque is adjustable. We set it for each of your cap types during installation, and your operator can adjust from there.
Probably — that’s what the positioning arrangement is for. Send us a bottle and we’ll run it before you order. Shape is harder to judge from a drawing than from the container itself.
On a shaped bottle, almost always because the container isn’t held squarely under the head. This machine’s holding arrangement addresses that, but it has to be configured to your specific bottle.
No. This machine stops for a missing bottle or a missing cap. Crooked-cap, reversed-cap and missing-liner rejection is on the APC-D902. If that check matters to you, tell us at the quotation stage.
Yes. We build to your U.S. supply at 60 Hz and confirm the voltage with your quote.
Yes. Our machines are certified and use certified electrical components. Because the exact scope depends on the model and electrical configuration you select, our factory confirms it in writing before production.
A kit of wear parts ships with your machine. Every part in the kit, and the lead time for anything outside it, is listed in your quote in writing.
Customers Also Interested In...
Send us your bottle and cap
We’ll run it on our own machine and send you a photo plus the torque readings. If your container is straightforward enough for a standard screw capper, we’ll tell you — it costs you less.
Send your line layout and we’ll show you where the capper fits and how much conveyor length you need either side.